Engineered Assemblies
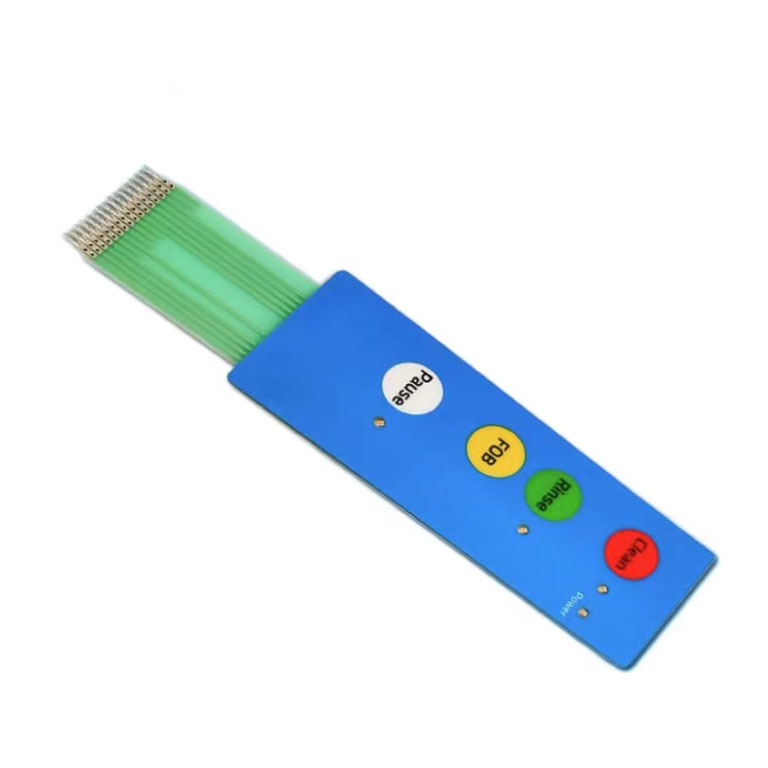
Featured Membrane Switch & Touch Interface Systems
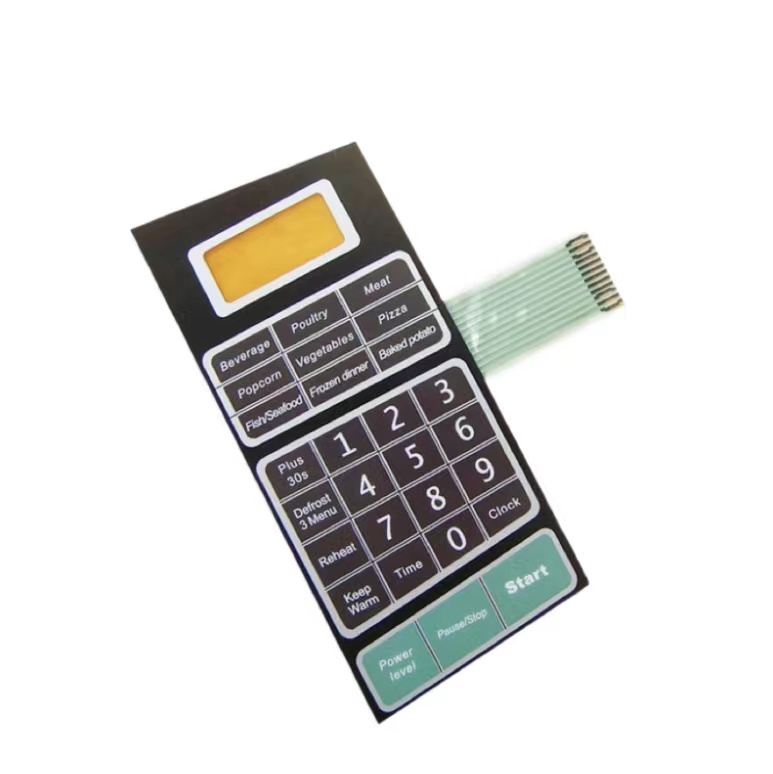
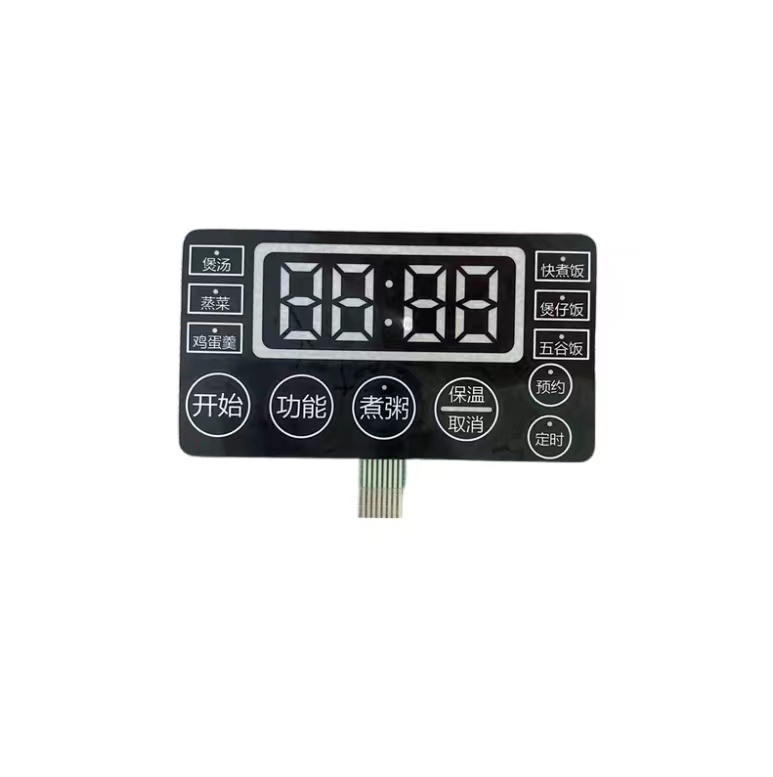
Tailor-made human-machine interface (HMI) configurations ready for immediate CAD/DFM integration, rigorous field duty, and extreme industrial environments across Andalusia.
Engineering Whitepaper Analysis
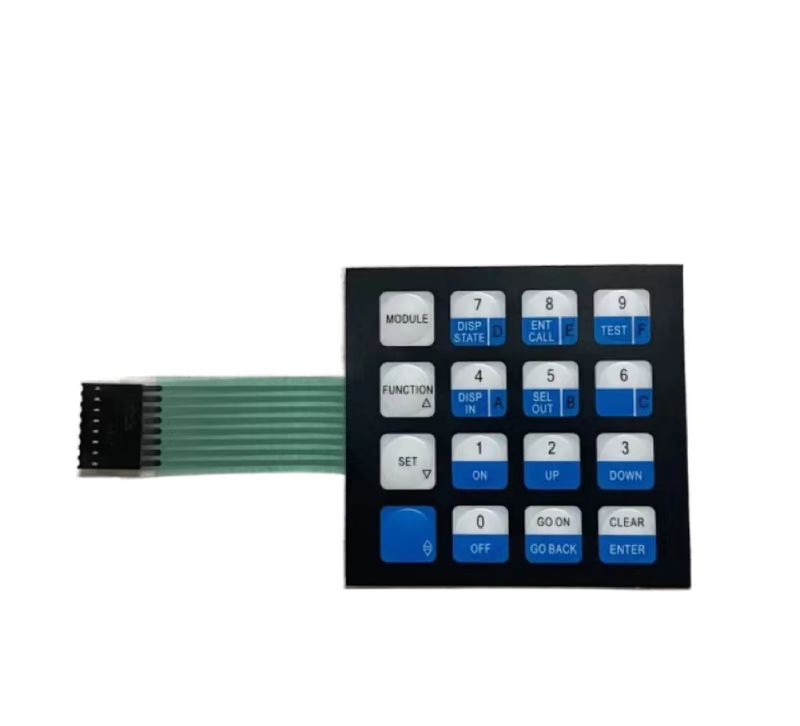
Layer Stack-Up Science: Demystifying Multi-Layer HMI Architecture
A granular technical breakdown of precision-screened, sub-surface printed membrane switches engineered for hostile thermodynamic and chemical operational windows.
Sub-Surface Graphic Layer
Fabricated using Autotex XE or fine-velvet polycarbonate, printed entirely in reverse on the second surface. This ensures keys, operational instructions, and corporate livery remain impervious to scratches, chemical wiping, abrasive sand, and hydraulic fluids.
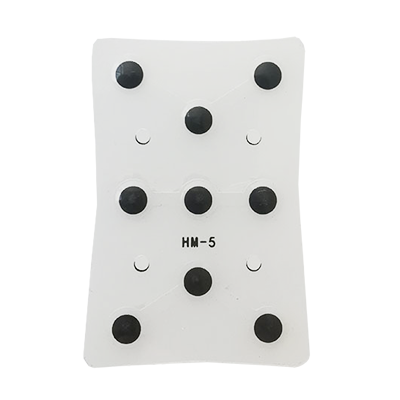
Tactile Snap Dome Arrays
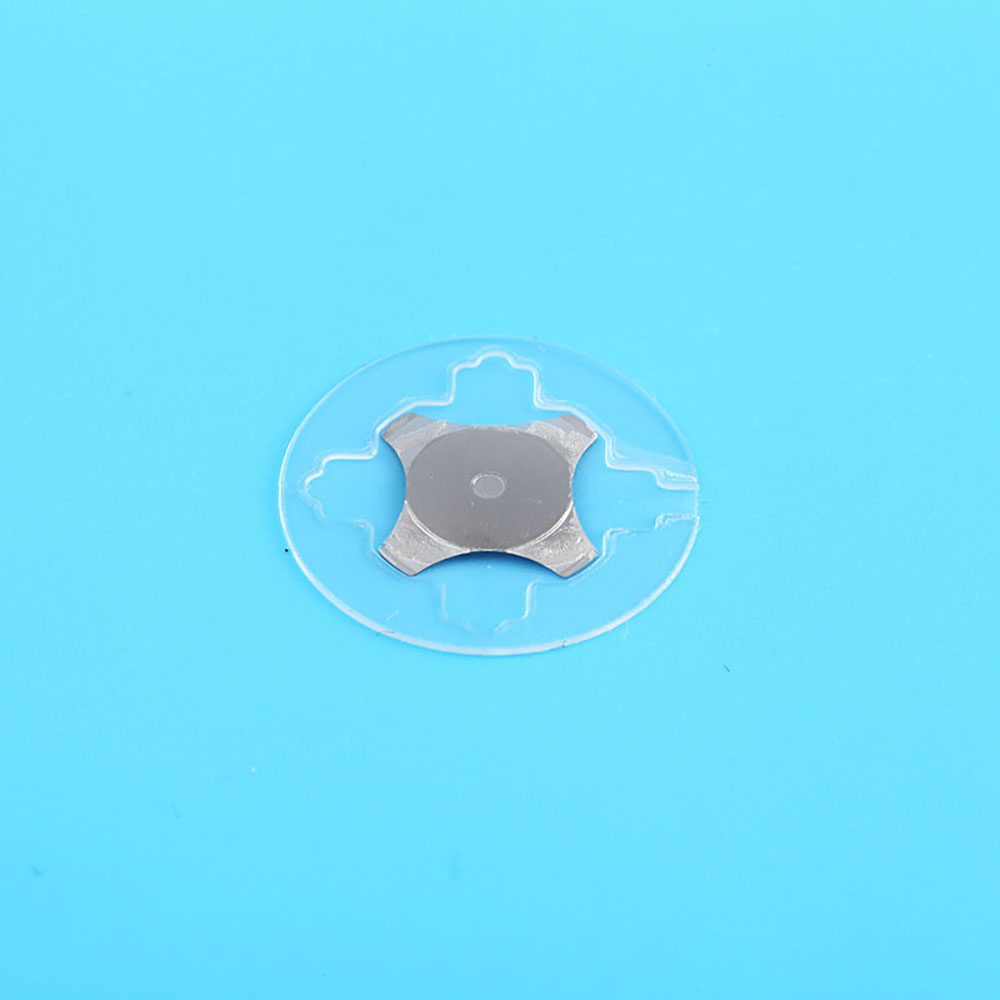
Utilizing high-tensile stainless steel (SUS301) with selective nickel or gold micro-plating. Delivers tactile feedback forces calibrated between 220g to 450g with trip-force tolerances strictly governed under ISO 9001 CCD vision and dome load verification.
Dielectric & Shielding Strata
Features ultra-stable silver conductive ink or double-sided polyimide flexible printed circuits (FPC). Integrated carbon-printed contact overcoats and etched copper/aluminum foil layers eliminate EMI/RFI noise and prevent silver migration in humid settings.
Anatomy of an Industrial-Grade Sealed Membrane Touch Interface
1. Graphic Overlay: 0.125mm – 0.200mm Autotex Polyester / UV Hard-Coated PC with anti-glare finish.
2. Graphic Adhesive: High-shear 3M 467MP / 3M 468MP acrylic adhesive transfer tape.
3. Dome Retainer Spacer: Custom-vented PET dielectric carrier accommodating 4-leg snap domes.
4. Circuitry Layer: Screen-printed polymer thick film (PTF) silver traces or photo-etched Cu-FPC tail.
5. Rear Gasket Mount: Modified acrylic 3M 300LSE adhesive bonding seamlessly to powder-coated cast aluminum.
Localized Industry Engineering
Seville & Andalusian Industrial Application Scenarios
How custom membrane touch panels empower tier-1 aerospace defense suppliers, concentrated solar installations, and agro-food automation systems in southern Spain.
Aerospace & Avionics GSE (Aerópolis)
Situated in the Aerópolis Aerospace Technology Park near Seville Airport, flight test equipment and Ground Support Equipment (GSE) require MIL-STD-810G compliant interfaces. Our membrane touch panels utilize non-reflective matte texturing, night-vision goggle (NVG) compliant backlighting, and FPC tails that endure high-g vibration profiles without intermittent contact disconnections.
Solar Thermal & Photovoltaic SCADA
From the PS10 and PS20 solar power towers in Sanlúcar la Mayor to large-scale PV tracker arrays throughout the Guadalquivir valley, localized control enclosures face extreme thermal cycles up to +50°C and relentless UV bombardment. Cevra integrates anti-yellowing UV stabilizers and high-temperature acrylic bonding films rated from -40°C to +85°C continuous service.
Agro-Food & Olive Oil Bottling Automation
In the vast agro-industrial zones spanning Alcalá de Guadaíra, Dos Hermanas, and Seville proper, olive oil centrifuges and wine bottling bottling machinery undergo daily chemical washdowns. Our seamless capacitive PMMA panels and sealed membrane switches achieve complete IP67 washdown ingress sealing, resisting caustic detergents and preventing organic oil migration.
Strategic Market Evolution
Seville Industrial Transition & HMI Modernization Trends
Aligning component manufacturing with the southern European digital shift toward Industry 4.0, hygienic interfaces, and circular economic compliance.
Migration from Mechanical Buttons to Capacitive PMMA
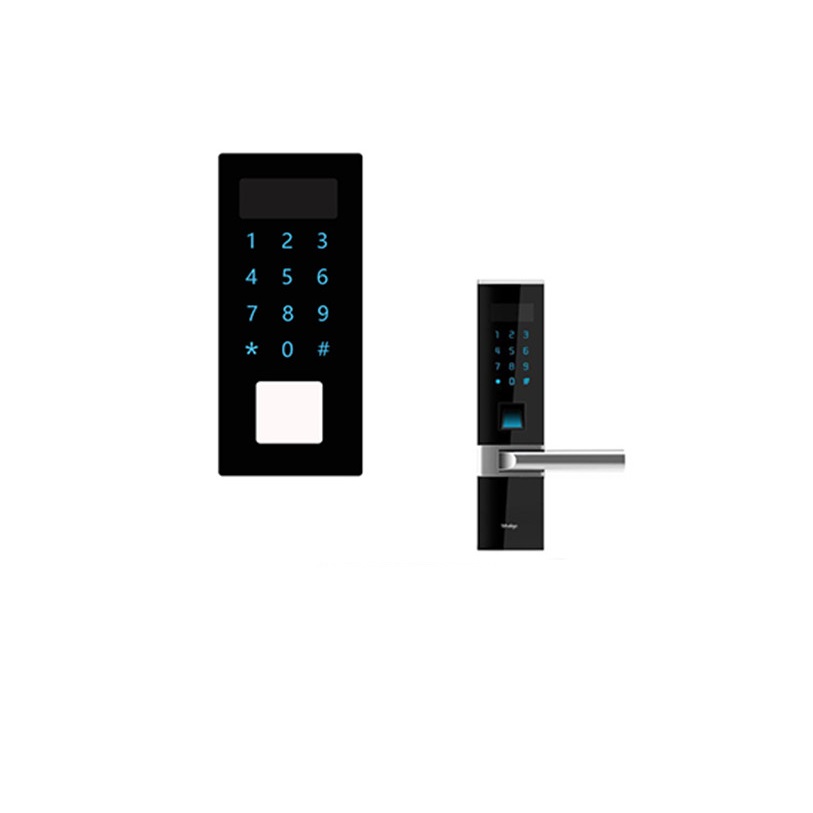
Manufacturing plants across Seville are replacing mechanical pushbuttons with unbroken acrylic (PMMA) capacitive touch consoles. Eliminating mechanical crevices stops particulate accumulation, lowers maintenance overhead, and facilitates cleanroom-level hygiene in biomedical research labs located within Cartuja Science and Technology Park (PCT Cartuja).
Light Guide Film (LGF) Uniformity Demands
Legacy individual LED arrays consume excessive space and suffer from localized hotspots. Modern Spanish industrial buyers are pivoting toward ultra-thin (0.125mm) Light Guide Film (LGF) modules powered by low-draw side-fire SMD LEDs, distributing light evenly across complex warning matrices while conserving power in battery-backed off-grid enclosures.
Eco-Design Directives & Material Traceability
Strict European Union environmental frameworks (EU RoHS Directive 2011/65/EU and REACH Regulation EC 1907/2006) require full raw material transparency. Seville's industrial OEMs mandate supply chain auditing that eliminates hazardous halogen flame retardants, hexavalent chromium, and phthalate plasticizers from export membrane products.
| Evaluation Parameter | PET Tactile Dome Panel | Capacitive PMMA Touch Glass | FPC Metal Dome Array Sheet |
|---|---|---|---|
| Tactile Response | Audible, distinct click (SUS Snap Dome) | Haptic vibration, LED or chime feedback | Short-travel, high-snap mechanical feel |
| Washdown & Sealing | IP65 – IP67 (Continuous Perimeter Gasket) | IP68 / IP69K (Hermetic Monolithic Face) | Dependent on housing enclosure seal |
| Direct Solar / UV Tolerance | Autotex XE UV polyester recommended | Exceptional optical PMMA stability | Protected beneath sub-surface bezel |
| Connector Tail System | 2.54mm / 1.00mm Pitch CrimpFlex or ZIF | High-density FPC / I2C / SPI Controller | Direct SMD soldering or surface mount array |
| Operating Lifecycle | > 1,000,000 actuations | > 5,000,000 touch cycles | > 1,000,000 actuations |
Enterprise Strengths
Why European Procurement Teams Trust Dongguan Cevra
A dedicated manufacturing plant, verified on-site by SGS Group, integrating every phase of design, production, cleanroom assembly, and laboratory QA.
ISO 9001 & SGS Audited
Operating since March 2009 in Dongguan, our 2,600㎡ production facility is governed under a strict ISO 9001 quality system and independently authenticated on-site by SGS Group, ensuring certified compliance with CE, RoHS, and REACH international protocols.
100% In-House Processing
No outsourcing shortcuts. We control the entire production pipeline: precision screen printing, automated laminating, CCD visual drilling, pneumatic die-punching, CNC laser profiling, and automated snap dome placement stations.
Rigorous QA Laboratory Testing
Every batch is subjected to dome load testers for click-ratio verification, peel-tension testers, tack testing, electric pencil hardness abrasion verification, and automated high/low temperature humidity cycle chambers (-40°C to +105°C).
Zero Tooling Lock-In
Flexible prototypes from 10 pcs; scaled runs to 100,000+ units.
Direct DFM Engineering
Comprehensive layout review, layer stack-up guidance & color matching.
Trade Assurance Protection
Secure international cross-border transactions and verified dispatch schedules.
Procurement Knowledge Base
Frequently Asked Questions by Seville & Spanish Buyers
Key commercial, technical, and logistic insights for procurement officers, system integrators, and design engineers sourcing custom membrane panels.
How do Cevra membrane panels handle Seville's intense summer heat and UV exposure?
Seville experiences sustained summer temperatures exceeding +42°C, coupled with intense solar UV irradiation. For exterior installations (such as solar trackers, smart municipal kiosks, and agricultural sensors), we specify premium Autotex XE polyester films or UV-stabilized polycarbonate treated with hard-coat resins. These substrates prevent embrittlement, blistering, and yellowing. Combined with 3M 200MP or 300LSE acrylic adhesives, our panels maintain full peel cohesion under extended thermal cycles from -40°C to +85°C.
What engineering documentation is required to receive a formal DFM review and quotation?
To provide an accurate technical quote and design-for-manufacture (DFM) assessment within 24 hours, our engineering office requires:
- Vector graphic overlay files (Adobe Illustrator .AI, .EPS, or .PDF) with color codes specified in Pantone matching system (PMS) or RAL.
- Mechanical dimensions and cut-out profiles in 2D vector CAD (.DXF or .DWG).
- Schematic pin-out wiring schedule, tail length, and connector termination type (such as 2.54mm Nicomatic female housing, solder tabs, or ZIF contacts).
- Operational preferences: tactile feel with metal snap domes, non-tactile embossing, LGF backlighting, or integrated surface-mount indicator LEDs.
How are import tariffs, VAT, and customs clearance handled when exporting to Spain?
As an experienced direct exporter to the European Union, Cevra provides complete documentation according to Spanish Customs regulations (Agencia Tributaria). Shipments utilize international HS codes 8537.10 (electrical control panels) or 8536.50 (switches). We offer flexible Incoterms including EXW, FOB Shenzhen/Hong Kong, CIF Port of Algeciras or Valencia, or DDP (Delivered Duty Paid) via DHL/FedEx Express air-freight directly to your receiving dock in Seville, managing Spanish customs clearance and IVA administration.
Can you match specific Pantone corporate colors and guarantee backlighting uniformity?
Yes. Our printing facility operates automated silk-screen presses and utilizes spectrophotometric color-matching systems to align with Pantone and RAL palettes. For backlighting, we deploy precision Light Guide Films (LGF) paired with computer-simulated micro-dot diffusers. This guarantees uniform light extraction across key legends without the shadows or uneven luminescence typical of simple edge-LED setups.
What are your prototyping MOQs, tooling costs, and production lead times?
We support fast-iteration product development. Graphic overlay and prototype keypad sample batches start as low as 10 to 50 pieces using digital printing and CNC plotter cutting, eliminating high tooling commitments. For full volume production runs:
- Rapid Prototyping: 7 to 10 working days from design proof approval.
- Standard Tooling: Steel rule dies and circuit printing plates prepared in 5 days.
- Mass Production: 2 to 3 weeks for quantities ranging from 500 to 50,000+ units, air-freighted directly to Andalusia.
Start Your Custom HMI Project
Ready to Engineer Your Seville Custom Membrane Assembly?
Connect directly with our senior HMI application engineering team. Send us your CAD drawings or technical requirements for immediate DFM feedback, stack-up optimization, and a detailed price proposal within 24 hours.