High-Reliability Capacitive Membrane Switches & Tactile Assemblies
Explore our export-grade Human-Machine Interface technologies manufactured specifically to withstand rugged operations, moisture, chemical washdowns, and continuous heavy-cycle actuation.
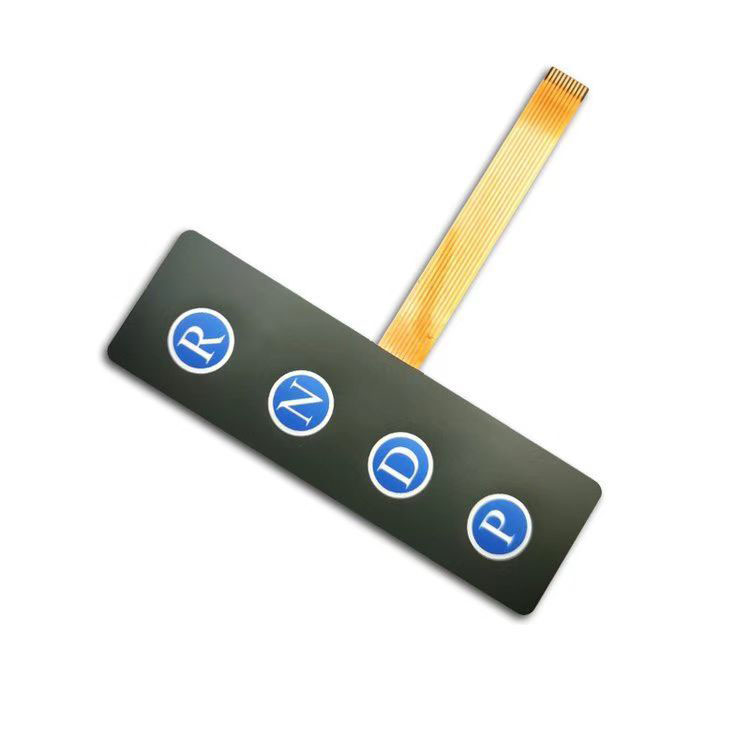
Embossing DIY Backlit 3 4 5 Button Touch Controller
- Technology: Capacitive / Backlit LED
- Overlay: Embossed Polycarbonate
- Ingress: IP65 / IP67 Compliant
- Application: Custom Retrofit & Lab Gear
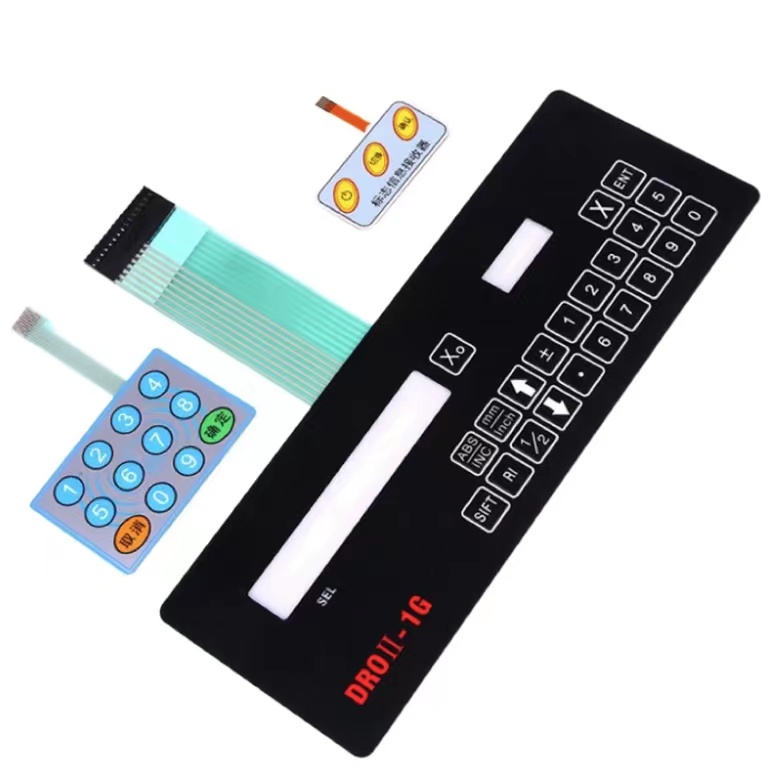
Factory Direct Graphic Overlay Custom Membrane Keyboard
- Substrate: Autotex Hard-Coated PET
- Adhesive: 3M 467MP / 3M 468MP
- Printing: High-Precision Silkscreen
- Application: Heavy Industrial Terminals
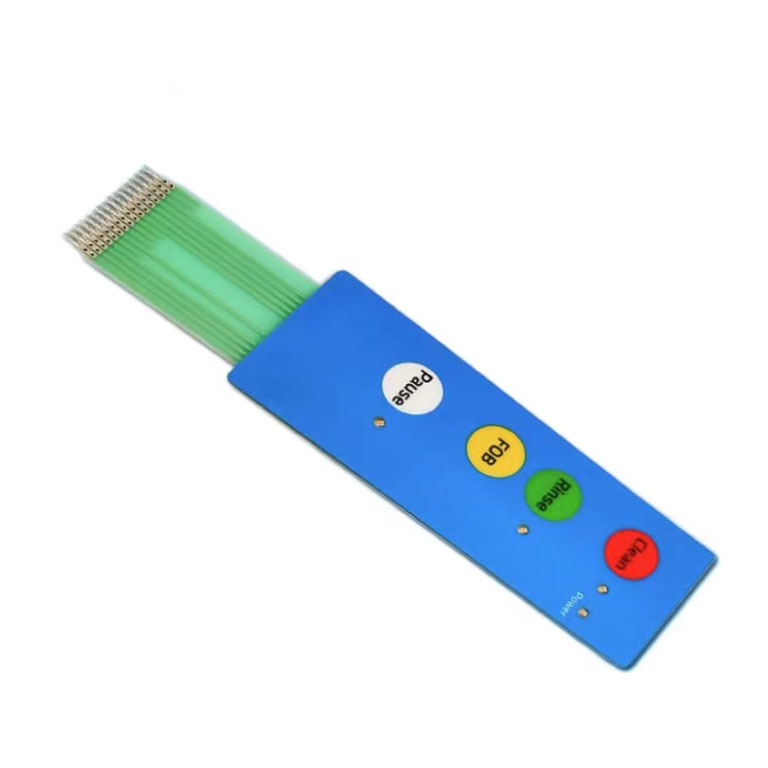
Waterproof Electronic Film Circuit Membrane Switch
- Circuitry: Silver Conductive Trace
- Flexibility: Ultra-Thin Flexible PET
- Resistance: < 1 Ohm/cm Conductance
- Application: Compact Consumer & Wearables
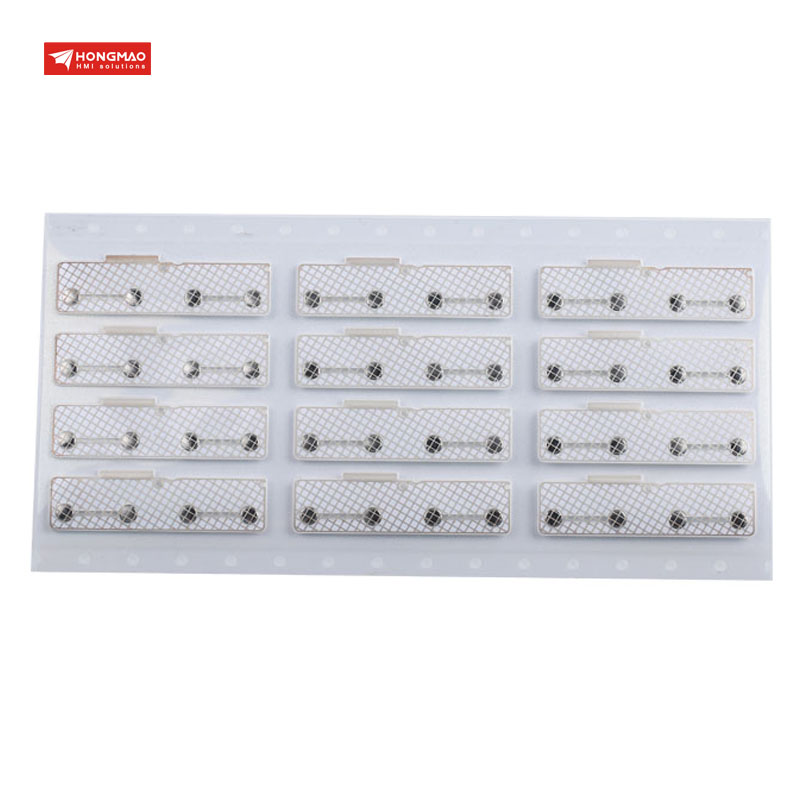
Double-Sided SUS301 Stainless Steel EMI Dome Array
- Material: SUS301 Stainless Steel
- Shielding: Integrated EMI / ESD Layer
- Tactile Force: Custom 250g - 450g
- Application: Avionics & Mining Controllers
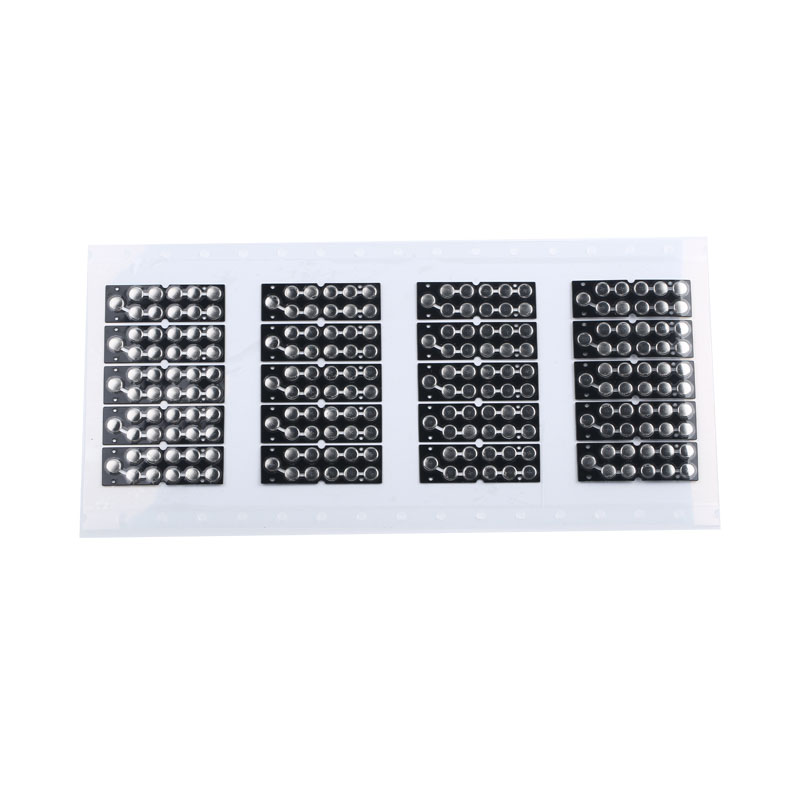
Round Metal Dome Array Single Layer Transparent PET
- Carrier: Optical Grade Transparent PET
- Plating: Nickel / Gold Plated
- Actuation: Crisp Tactile Snap Feel
- Application: Handheld Scanners & Remotes
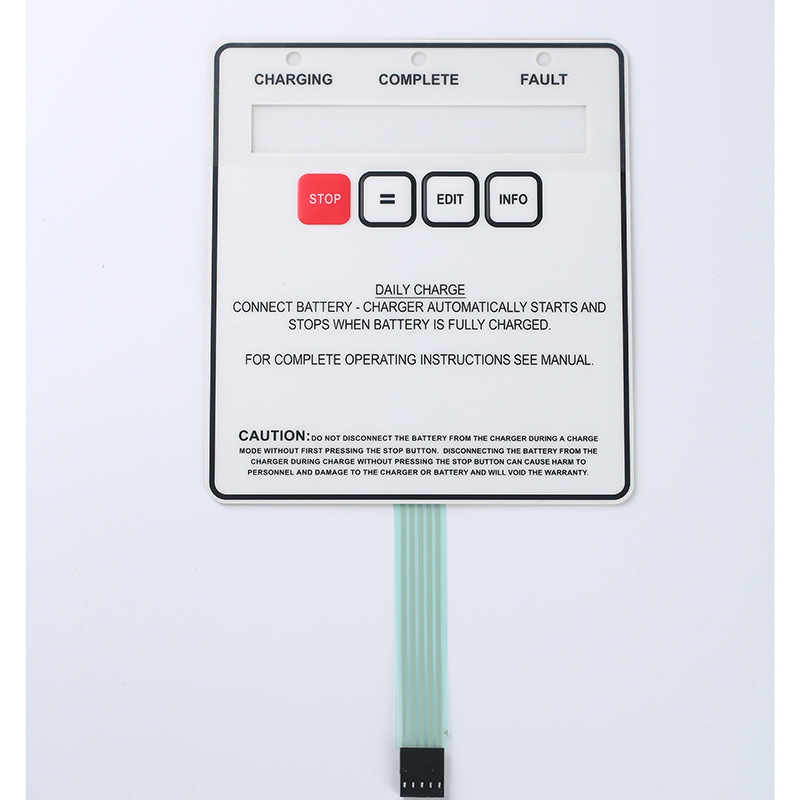
Medical Equipment Waterproof Membrane Control Panel
- Cleanability: Hospital Disinfectant Proof
- Sealing: Full IP67 Perimeter Barrier
- Compliance: Biocompatible Overlay Film
- Application: Diagnostic & Surgical Devices
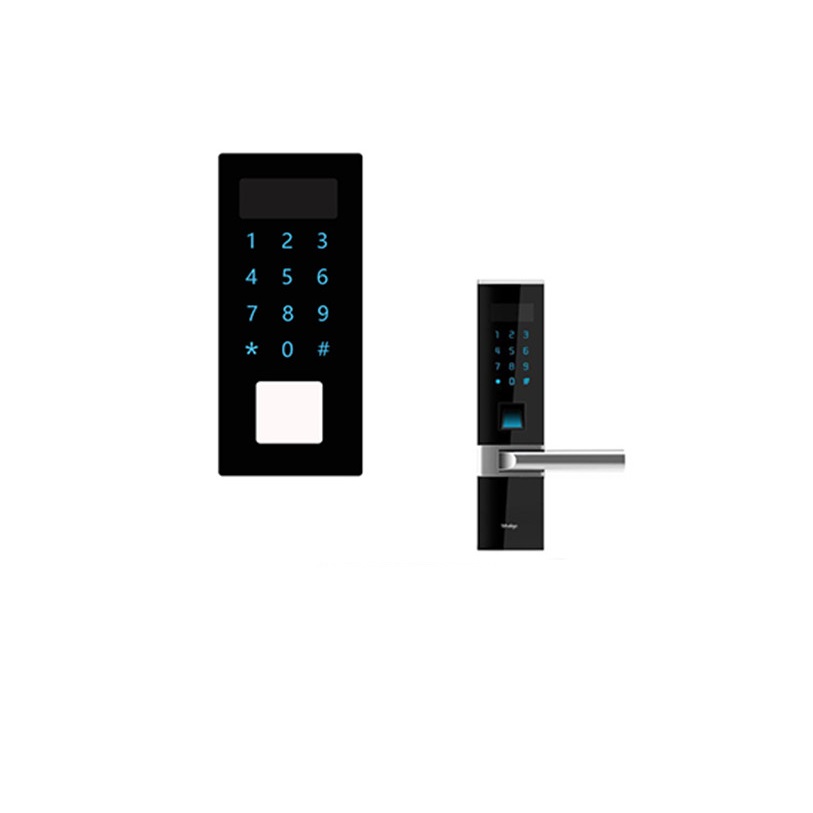
Custom PMMA Smart Capacitive Touch Switch Keypad
- Fascia: PMMA Acrylic / Glass-Like
- Sensing: Solid-State Capacitive Touch
- Connector: FPC Pitch 0.5mm / 1.0mm
- Application: Smart Access & Building Tech
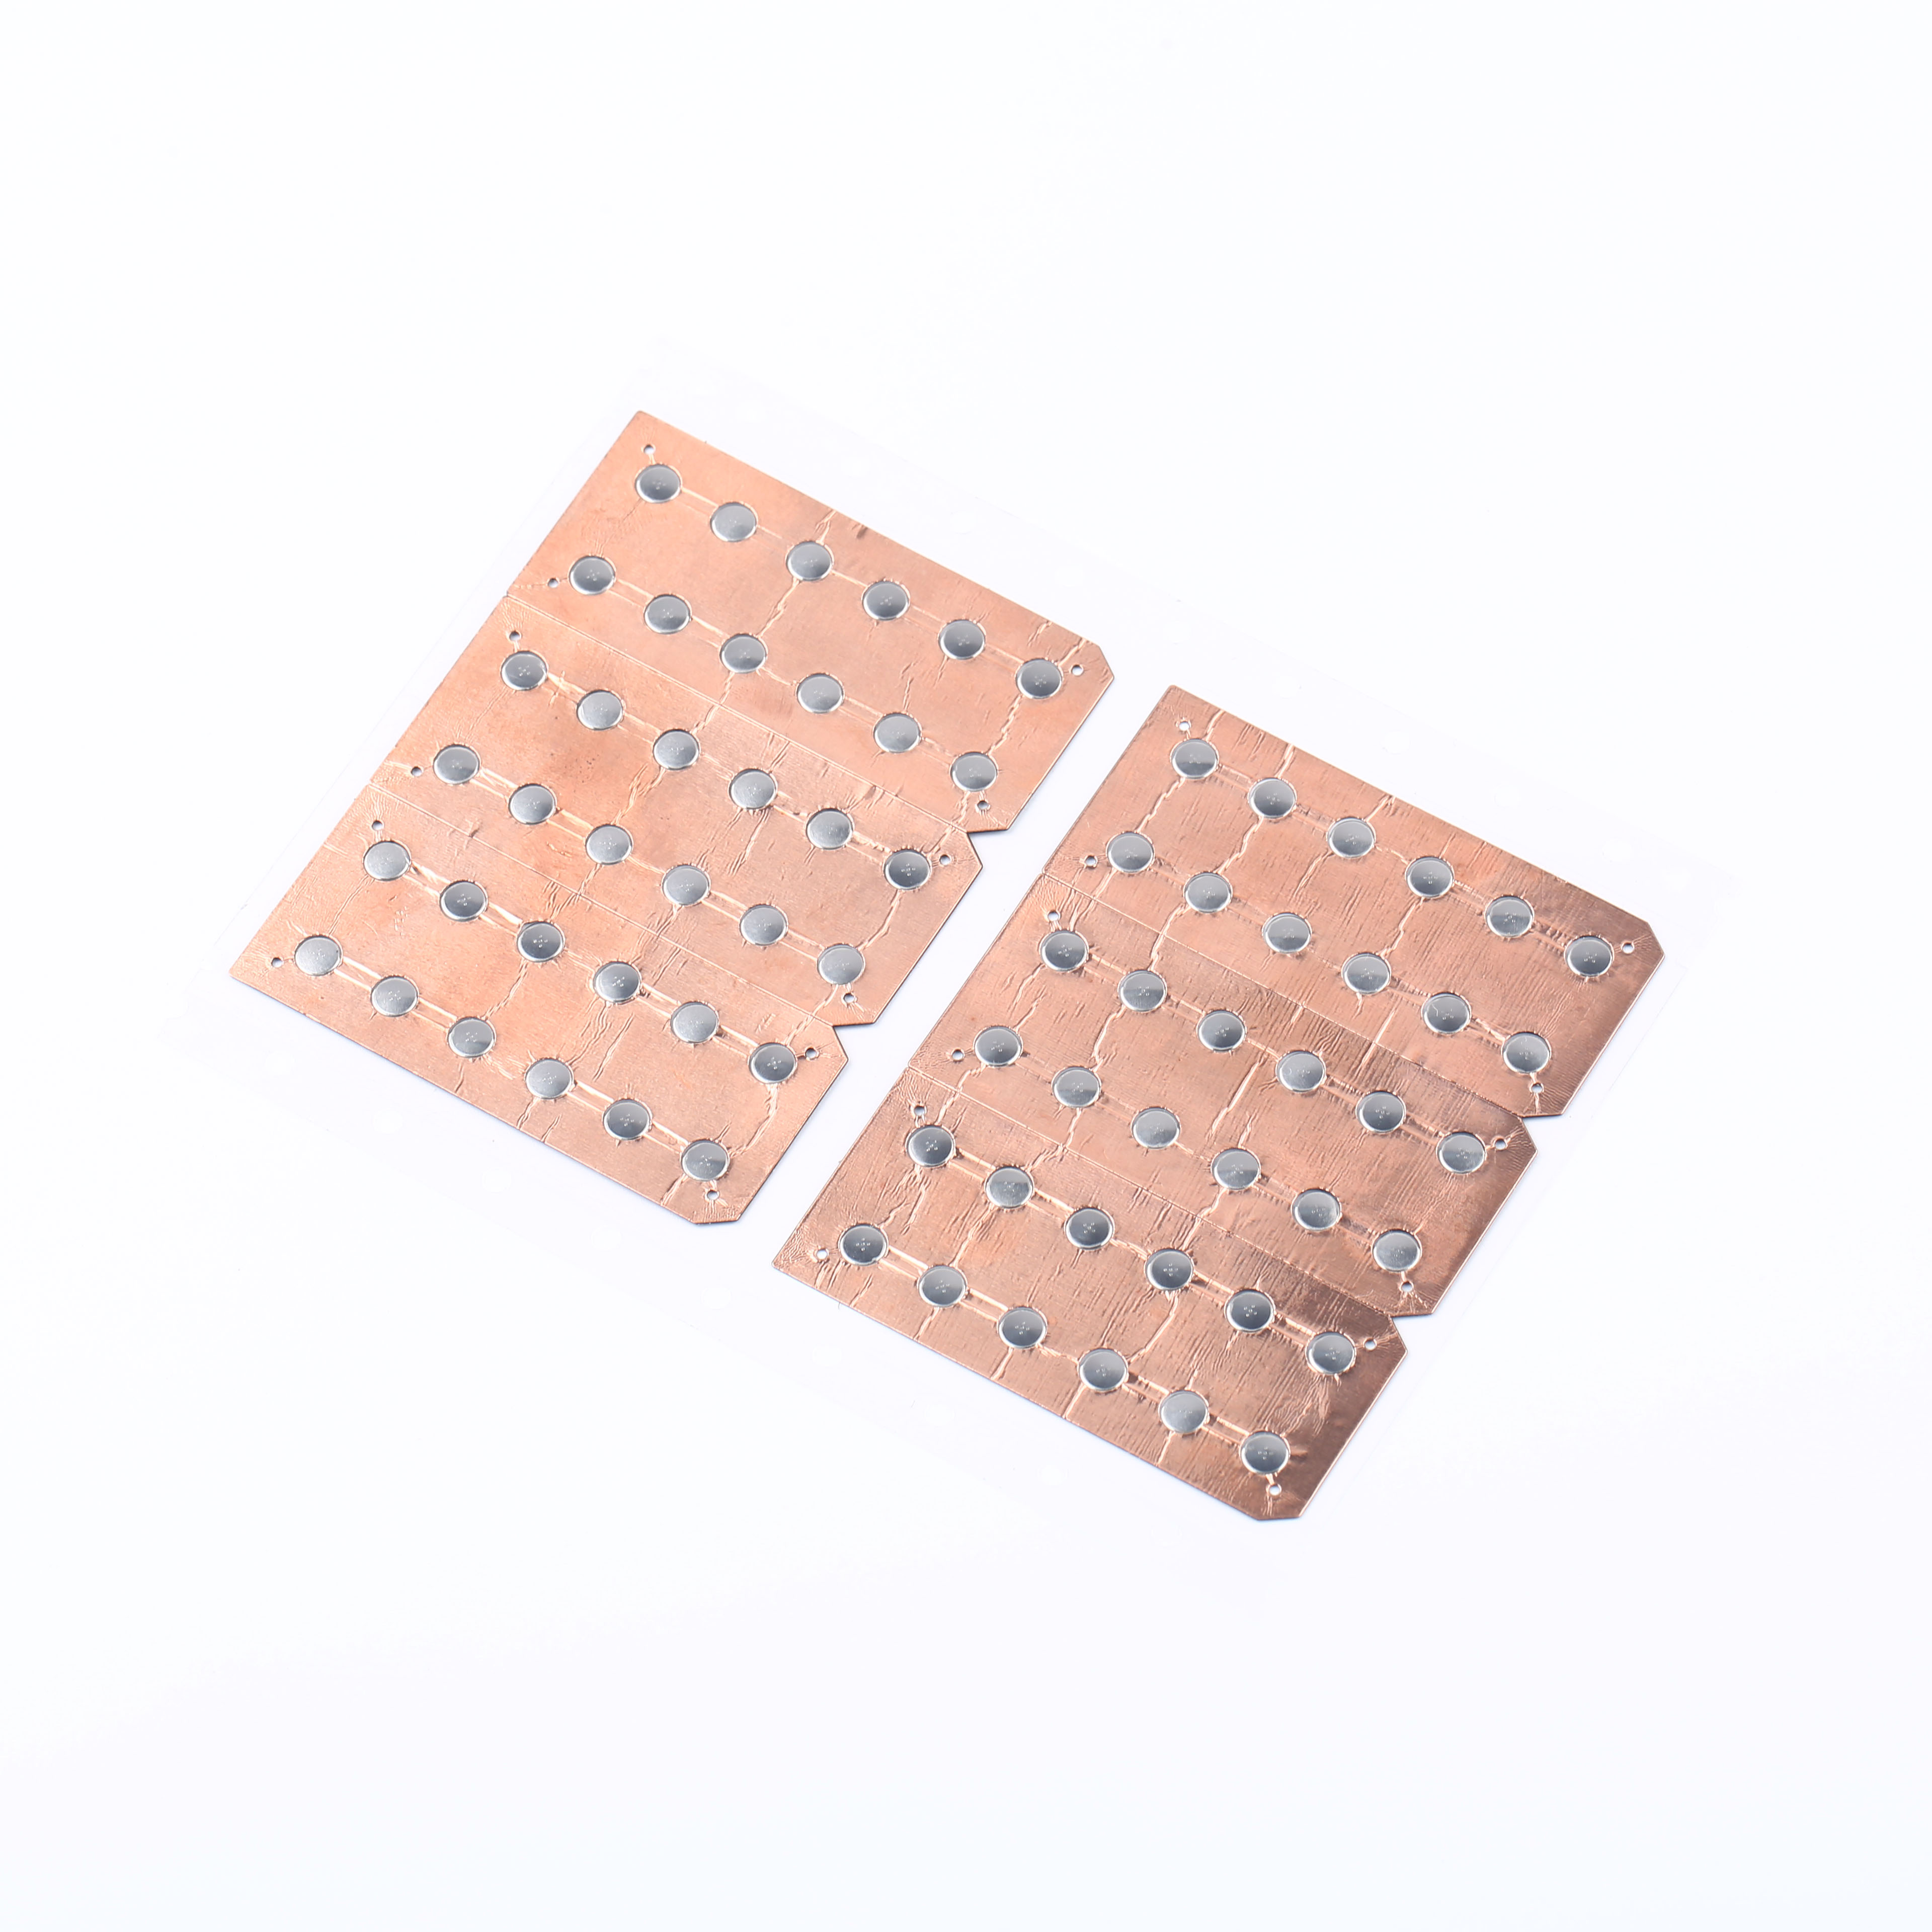
Copper Foil Metal Snap Dome Array Carrier Sheet
- Backer: High Conductive Copper Foil
- Dome Type: 4-Leg Cross / Circular Domes
- Assembly: Peel-and-Stick Fast Alignment
- Application: High-Density PCB Interfacing
Engineering Human-Machine Interfaces for Victoria's High-Tech Industries
From the automated processing corridors of Greater Melbourne to heavy industrial testing in Geelong, our capacitive switches fulfill demanding technical environments.
MedTech Hub: Parkville & Clayton Corridors
Victoria's medical device developers require clinical interfaces capable of surviving hospital-grade sanitation protocols, autoclaves, and aggressive wipes like isopropyl alcohol and bleach. Our solid-state capacitive touch panels utilize completely seamless, non-porous polyester overlays that eliminate fluid ingress, particulate accumulation, and microbial growth vectors.
AgTech & Food Processing: Goulburn Valley
Irrigation management nodes, sorting electronics, and vineyard automation panels deployed throughout regional Victoria battle extreme temperature swings and high-pressure chemical washdowns. We engineer wide-temperature (-40°C to +85°C) UV-stabilized graphic skins matched with IP67 potted perimeter adhesives to prevent delamination under baking Australian sun.
Heavy Industry: Dandenong & Geelong Manufacturing
Heavy machinery, rail transport, and defense component manufacturers demand HMIs impervious to vibration, grease, and electromagnetic interference (EMI). Our integrated copper/aluminum ground shielding layers shield sensitive sensor traces against transient noise, delivering false-trigger rejection even in electrically noisy industrial plants.
Technical Whitepaper: Capacitive Sensing Paradigms in Modern Australian Hardware
In the transition toward Industry 4.0, product developers in Melbourne and regional Victoria are shifting away from traditional mechanical push-buttons in favor of solid-state capacitive membrane panels. Unlike traditional membrane switches that depend on physical contact closing through an air gap, capacitive switches operate by detecting changes in electrical capacitance when a conductive object (such as a human finger) approaches the dielectric overlay field.
This physical architecture provides distinct competitive advantages for Victoria's export-oriented OEMs: mechanical wear is virtually zero, moving mechanical parts are eliminated, and lifecycle counts easily exceed 5 million cycles without switch fatigue. Furthermore, by pairing etched indium tin oxide (ITO) or high-conductivity screen-printed silver paths on flexible polyethylene terephthalate (PET) with microprocessor-controlled tuning, capacitive keypads can be configured to sense through front panels up to 6mm thick—including vandal-resistant PMMA, polycarbonate, or toughened optical glass.
Water rejection algorithms engineered into the circuit layout guarantee that fluid pools, dew condensation, or saline cleansers will not generate phantom touches, satisfying stringent therapeutic goods and industrial safety expectations.
Why Victorian Engineers & Procurement Managers Partner with Cevra
We eliminate typical overseas supply chain frictions through verified technical capability, rapid direct DFM collaboration, and rigorous quality systems.
SGS Audited ISO 9001 Facility
Our 2,600㎡ Dongguan manufacturing site operates under ISO 9001 certified protocols, fully audited on-site by SGS Group. From optical raw material verification to computerized tensile testing, every production batch provides traceable dimensional and electrical integrity.
Direct-to-Engineer DFM Reviews
No sales middle-men. Victorian hardware teams work directly with senior HMI mechanical and electronic design engineers. We review layer stack-ups, switch pitch, tail termination, and backlighting mechanics within 24 hours of CAD/Gerber file receipt.
Agile Prototyping to High-Volume Runs
Victorian innovators require flexible initial trial runs before scaling. We support low-volume qualification batches starting from just 10 pieces for graphic overlays and 100 units for fully functional capacitive membrane switches, scaling easily into hundreds of thousands.
Comprehensive Environmental Testing
Our in-house QA lab runs peel tests, tactile life testing machines, pencil hardness tests (3H+ scratch resistance), and thermal cycling test chambers (-40°C to +105°C) to simulate decades of Australian field stress prior to overseas customs dispatch.
Global Export Ready Logistics
With direct air express dispatch to Melbourne Airport (MEL) and sea freight consolidations via Port of Melbourne, we offer transparent customs packaging, ESD-shielded vacuum bagging, and rapid air-transit times (3 to 5 business days).
End-to-End Vertical Control
We screen-print graphic facings, die-cut spacers, assemble tactile snap dome arrays, route FPC tails, and integrate Light Guide Films (LGF) or discrete SMD LEDs in-house. No outsourced quality compromises.
Frequently Asked Questions for Victorian Engineering Buyers
Key technical, commercial, and logistics considerations when sourcing capacitive touch membrane switches from our facility.