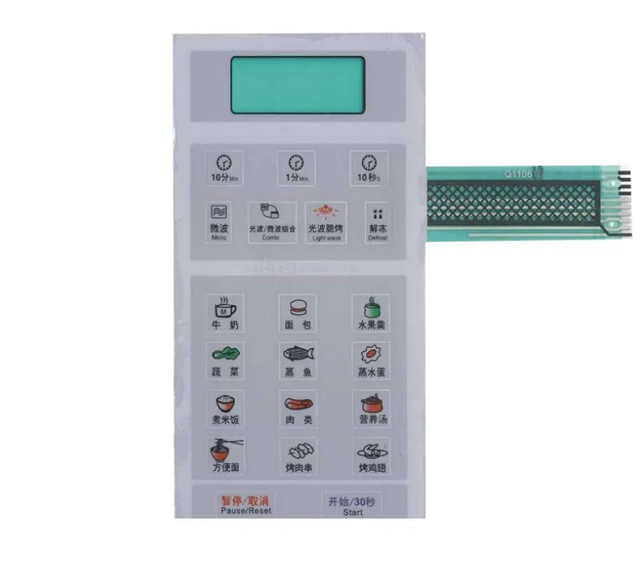
Factory Cheap Price Electronic Membrane Switch Membrane Switch Control Panel
- Tactile Feedback: SUS301 Metal Dome
- Sealing Standard: IP65 Ingress Protect
Direct-from-factory OEM precision manufacturing featuring ISO 9001 certified optical guide films, waterproof tactile metal domes, and robust graphic overlays tailored for remote installations.
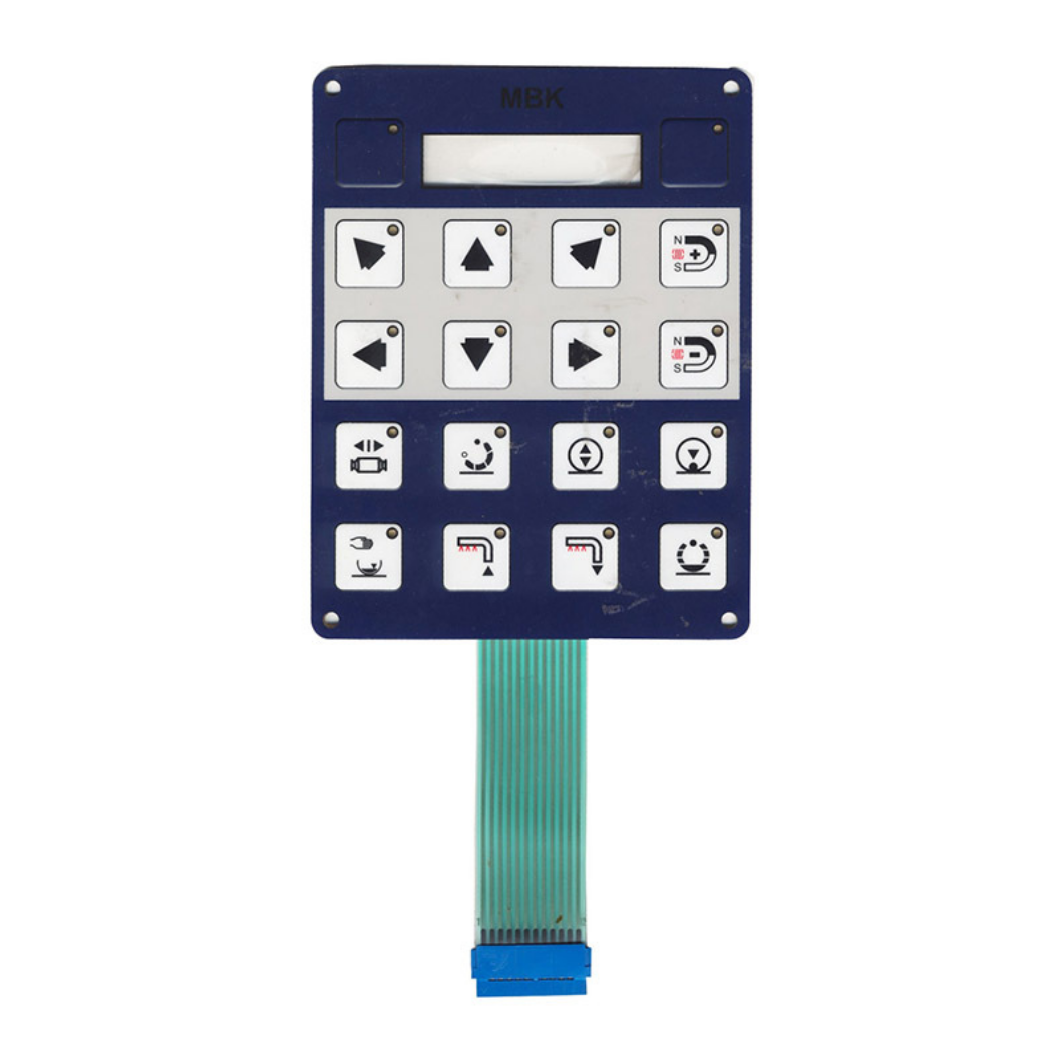
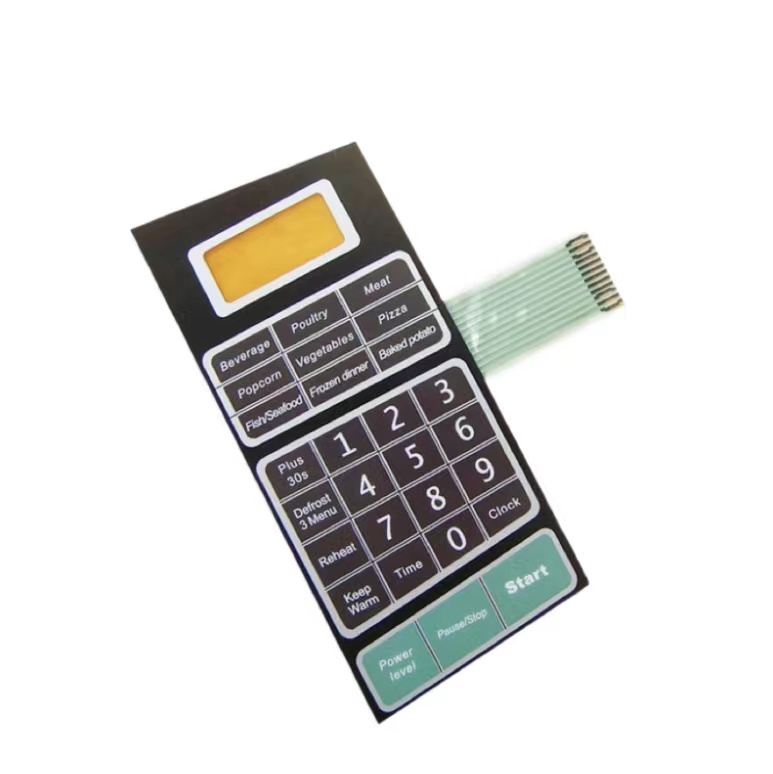
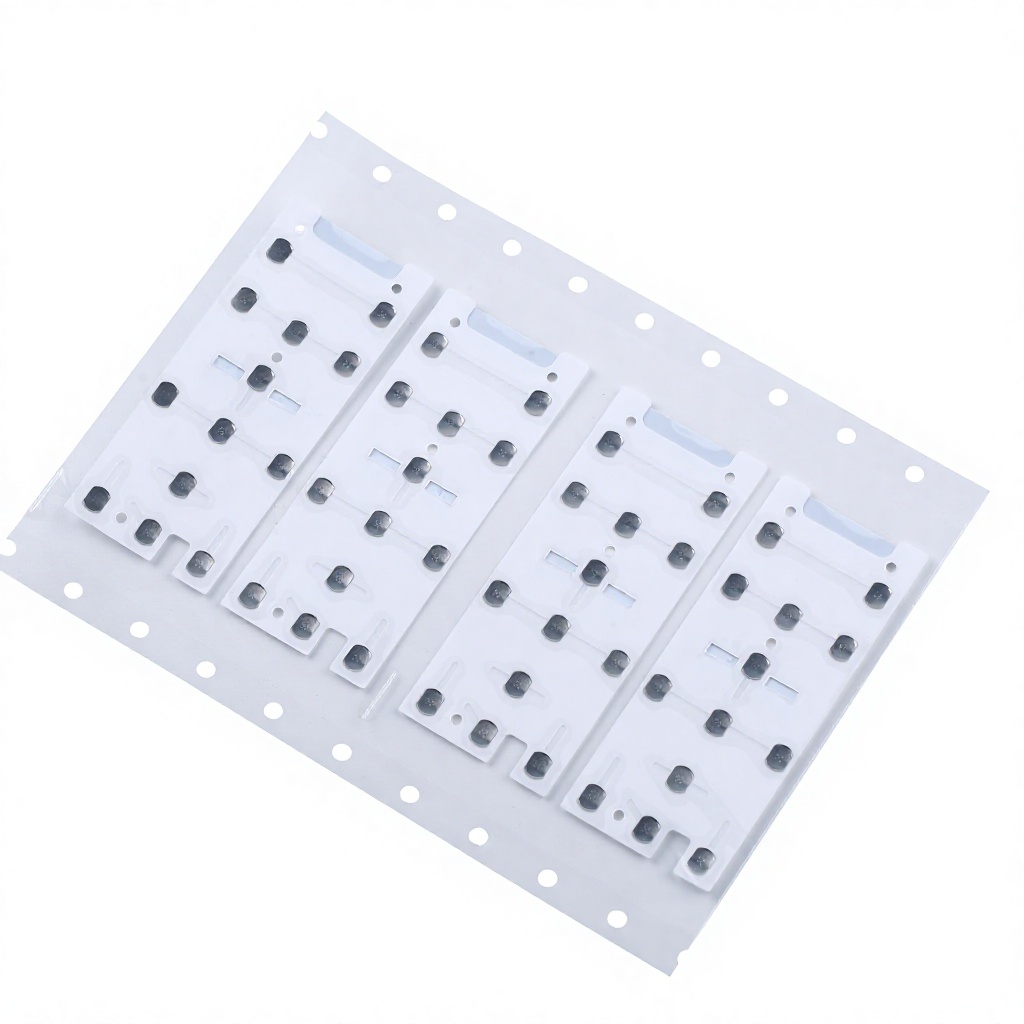
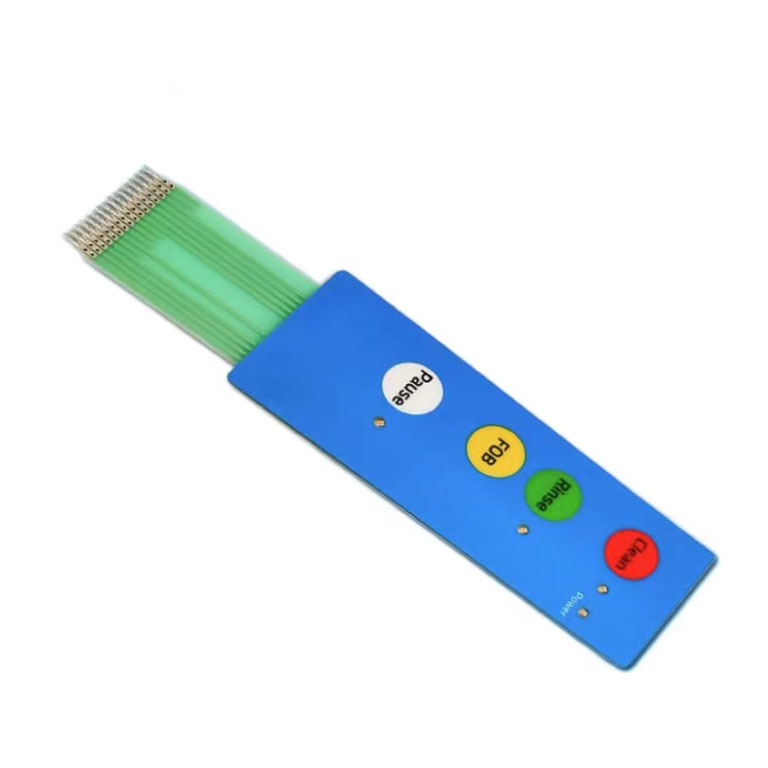
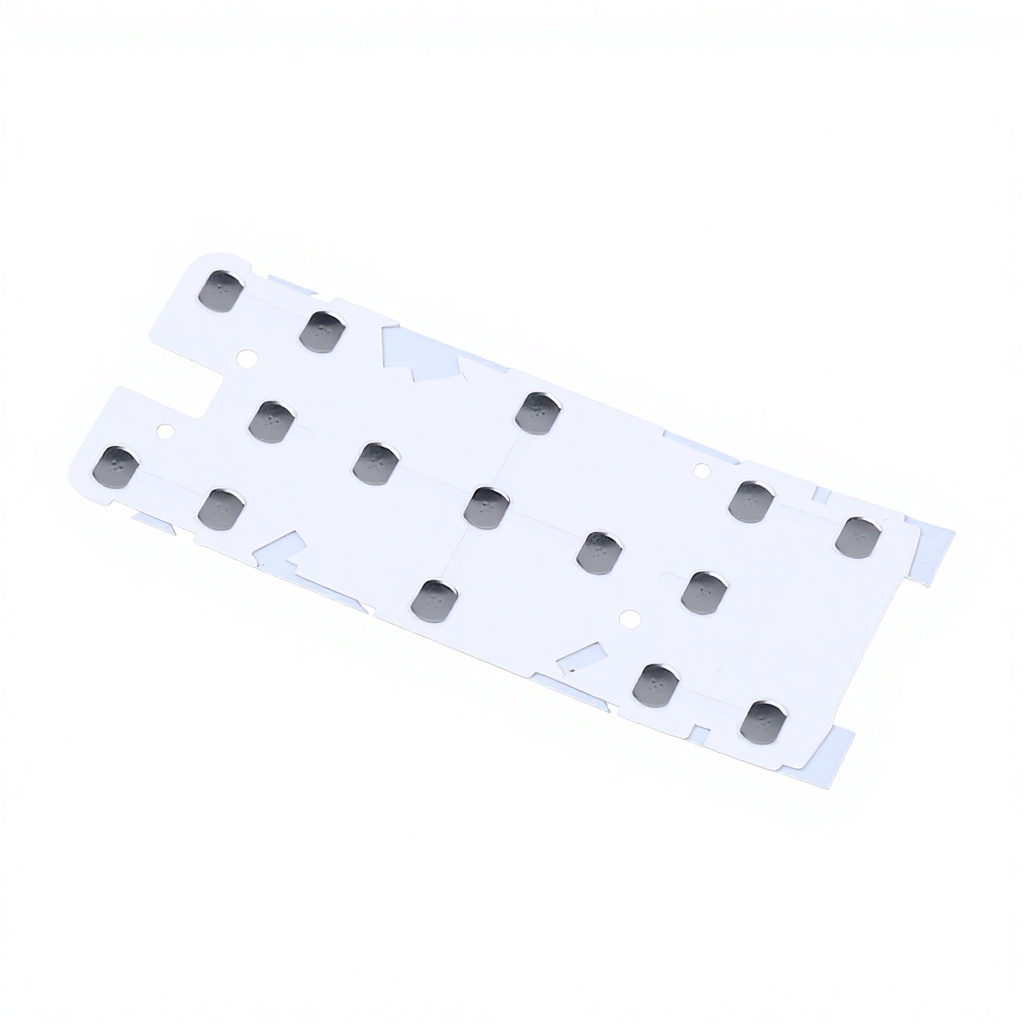
Operating industrial instrumentation in tropical, maritime environments requires components that resist aggressive atmospheric salinity, rapid temperature cycling, and high ultraviolet exposure. Asau—serving as a critical regional logistics point, deep-water port hub, and gateway for agricultural and emerging renewable energy infrastructure in Savaiʻi—demands human-machine interface (HMI) hardware that guarantees uninterrupted reliability under harsh oceanic conditions. Cevra delivers advanced Backlit Membrane Panel assemblies tailored precisely to mitigate corrosion, silver migration, and optical degradation caused by constant sea spray and relative humidity exceeding 85%.
Backlit membrane switches provide vital visual clarity during night operations, low-light marine bridge shifts, and enclosed diesel generator maintenance. When delivering backlit panels to maritime equipment operators and utility distributors serving Asau, selecting the appropriate optical dispersion substrate directly determines the panel’s electrical longevity and luminescence uniformity:
By coupling edge-mounted ultra-thin surface LEDs into a 0.125mm–0.25mm textured optical film, light is uniformly distributed across dead-front icons and legends without increasing switch travel distance or adding bulk to the front panel stack-up.
Direct placement of sub-miniature chip LEDs within custom spacer pockets enables individual key backlighting, status annunciation, and distinct color alerts (such as Amber fault states, Green operational indicators, and Blue active links).
Engineered for high-vibration engine bay compartments and boat consoles, these solutions deliver zero electromagnetic interference (EMI/RFI), providing a spark-free, non-arcing user interface for hazardous marine fuel pumping and storage zones.
Maritime ports and coastal processing facilities near Asau Bay face severe corrosion challenges. Standard commercial membrane keypads deteriorate rapidly in these settings due to moisture penetrating unsealed adhesive margins, which triggers electrochemical silver dendrite growth across parallel conductive traces. At Cevra, we address these environmental stresses using a multi-barrier defense strategy:
First, we apply an uninterrupted perimeter gasket utilizing medical-grade 3M 200MP/300LSE acrylic adhesives, establishing an IP67 hermetic barrier that locks out atmospheric water vapor and ocean spray. Second, our circuits feature fully encapsulated silver conductive traces protected by cured dielectric polymers and hydrophobic carbon ink barriers. For high-vibration boat throttles and wharf handling winches, our tactile layer incorporates SUS301 stainless-steel snap domes with nickel or selective gold plating to prevent micro-fretting corrosion, maintaining low contact resistance across more than 1,000,000 actuation cycles.
| Performance Characteristic | Commercial Grade Membrane Keypad | Cevra Backlit Maritime/Oceanic Spec |
|---|---|---|
| Operating Temperature | 0°C to +50°C (Interior use only) | -30°C to +85°C (Extreme tropical solar thermal load) |
| Relative Humidity Limit | 80% Non-Condensing | Up to 98% Relative Humidity (Hermetically sealed IP67/NEMA 4X) |
| Graphic Substrate Material | Standard Polycarbonate (PC) | Autotype XE Textured Marine-Grade Polyester (PET) |
| UV Resistance (Sunlight Exposure) | Degrades and yellows within 6–12 months | UV-stabilized > 5 years outdoor resistance against embrittlement |
| Tactile Dome Metallurgy | Untreated Stainless Steel / Bare Silver | Nickel/Gold-plated SUS301 with integrated breather channels |
Rather than providing generic electronic panels, our engineering team optimizes switch mechanics to match the real-world operational workflows of field engineers, vessel operators, and facility managers across Samoa's western island territory:
A. Harbor Marine Telemetry & Navigation Panels: Asau's historic channel and port operations demand sealed deck controls, bilge pump monitors, and chartplotter auxiliary keypads. Cevra builds night-vision compliant red and amber illuminated graphic overlays configured with wide tactile spacing, allowing deckhands wearing thick rubber gloves to actuate keys reliably with definite click confirmation.
B. Decentralized Microgrid & Solar Inverter Enclosures: With the Pacific transitioning aggressively toward distributed renewable energy systems, solar inverters and battery storage modules installed in coastal Savaiʻi run under high ambient temperatures. Our PET membrane overlays feature UV-resistant screen-printed formulations that prevent surface blistering, color bleaching, and tactile dome fatigue caused by relentless tropical sunlight.
C. Cold Chain Logistics & Agro-Industrial Processing: Timber handling, cocoa, and local agricultural cold-storage units require frequent high-pressure chemical washdowns. Cevra's PMMA capacitive touch panels and seamless embossed polyester membranes eliminate surface crevices, preventing bacterial harboring and water ingress during pressurized sanitation routines.
The Pacific Island trade region is increasingly turning to direct-from-manufacturer procurement models to streamline supply chains. Local infrastructure projects, commercial fleets, and engineering subcontractors serving Asau are adopting three key sourcing strategies:
Full-process in-house manufacturing based in Dongguan, providing direct technical accountability from initial layer stack-up review through final environmental qualification.
Operating since 2009, our 2,600㎡ facility undergoes rigorous onsite audits by the SGS Group. Every batch is manufactured under strict quality standards covering incoming material verification and lot traceability.
From screen printing and precision laser routing to automated laminating and CCD target drilling, all processes are executed internally. This vertical integration shortens lead times and ensures clean environmental controls.
Our in-house quality assurance laboratory verifies performance using computerized dome load testers, high/low thermal cycling cabinets (-40°C to +105°C), 180° adhesive peel gauges, and mechanical pencil hardness testers.
Common technical, logistics, and design feasibility questions answered by our engineering and export team.
Submit your CAD schematics, dimensional drawings, or project parameters. Our application engineering team will review your file for manufacturability (DFM) and deliver an itemized quotation within 24 hours.