16+ Years
HMI Manufacturing Prowess (Est. 2009)
2,600 ㎡
Class 1,000 Cleanroom Production
100% Tested
CCD Vision & Force Trip Profiling
>1,000,000
Actuations Guaranteed Lifespan
High-Reliability Metal Dome Arrays & Membrane Switches
Configured specifically for embedded systems, medical diagnostics, laboratory instruments, and industrial control consoles across County Limerick and Ireland's leading technology corridors.
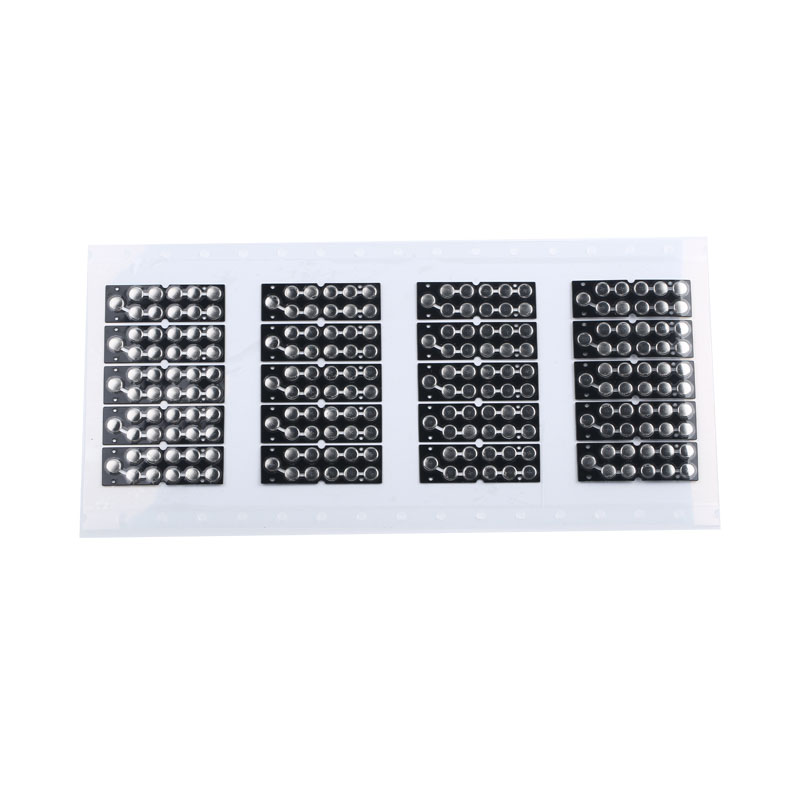
- Form Factor: Round Snap Dome
- Trip Force: 160g – 280g Customizable
- Base Film: Optically Clear PET
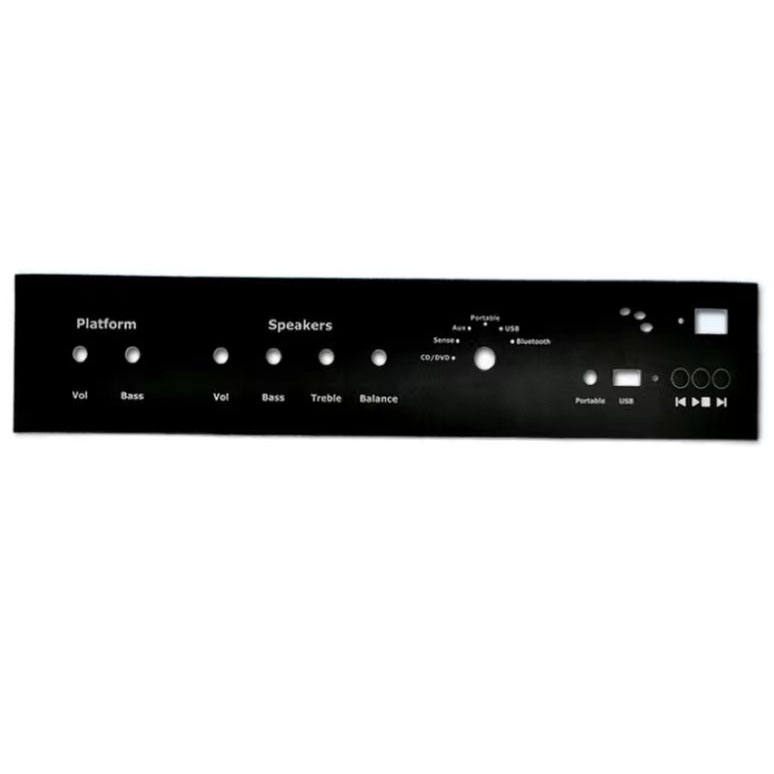
- Ingress Rating: IP65 / IP67 Water Sealed
- Surface Finish: Anti-Glare Textured PET
- Circuitry: Screen-Printed Conductive Silver
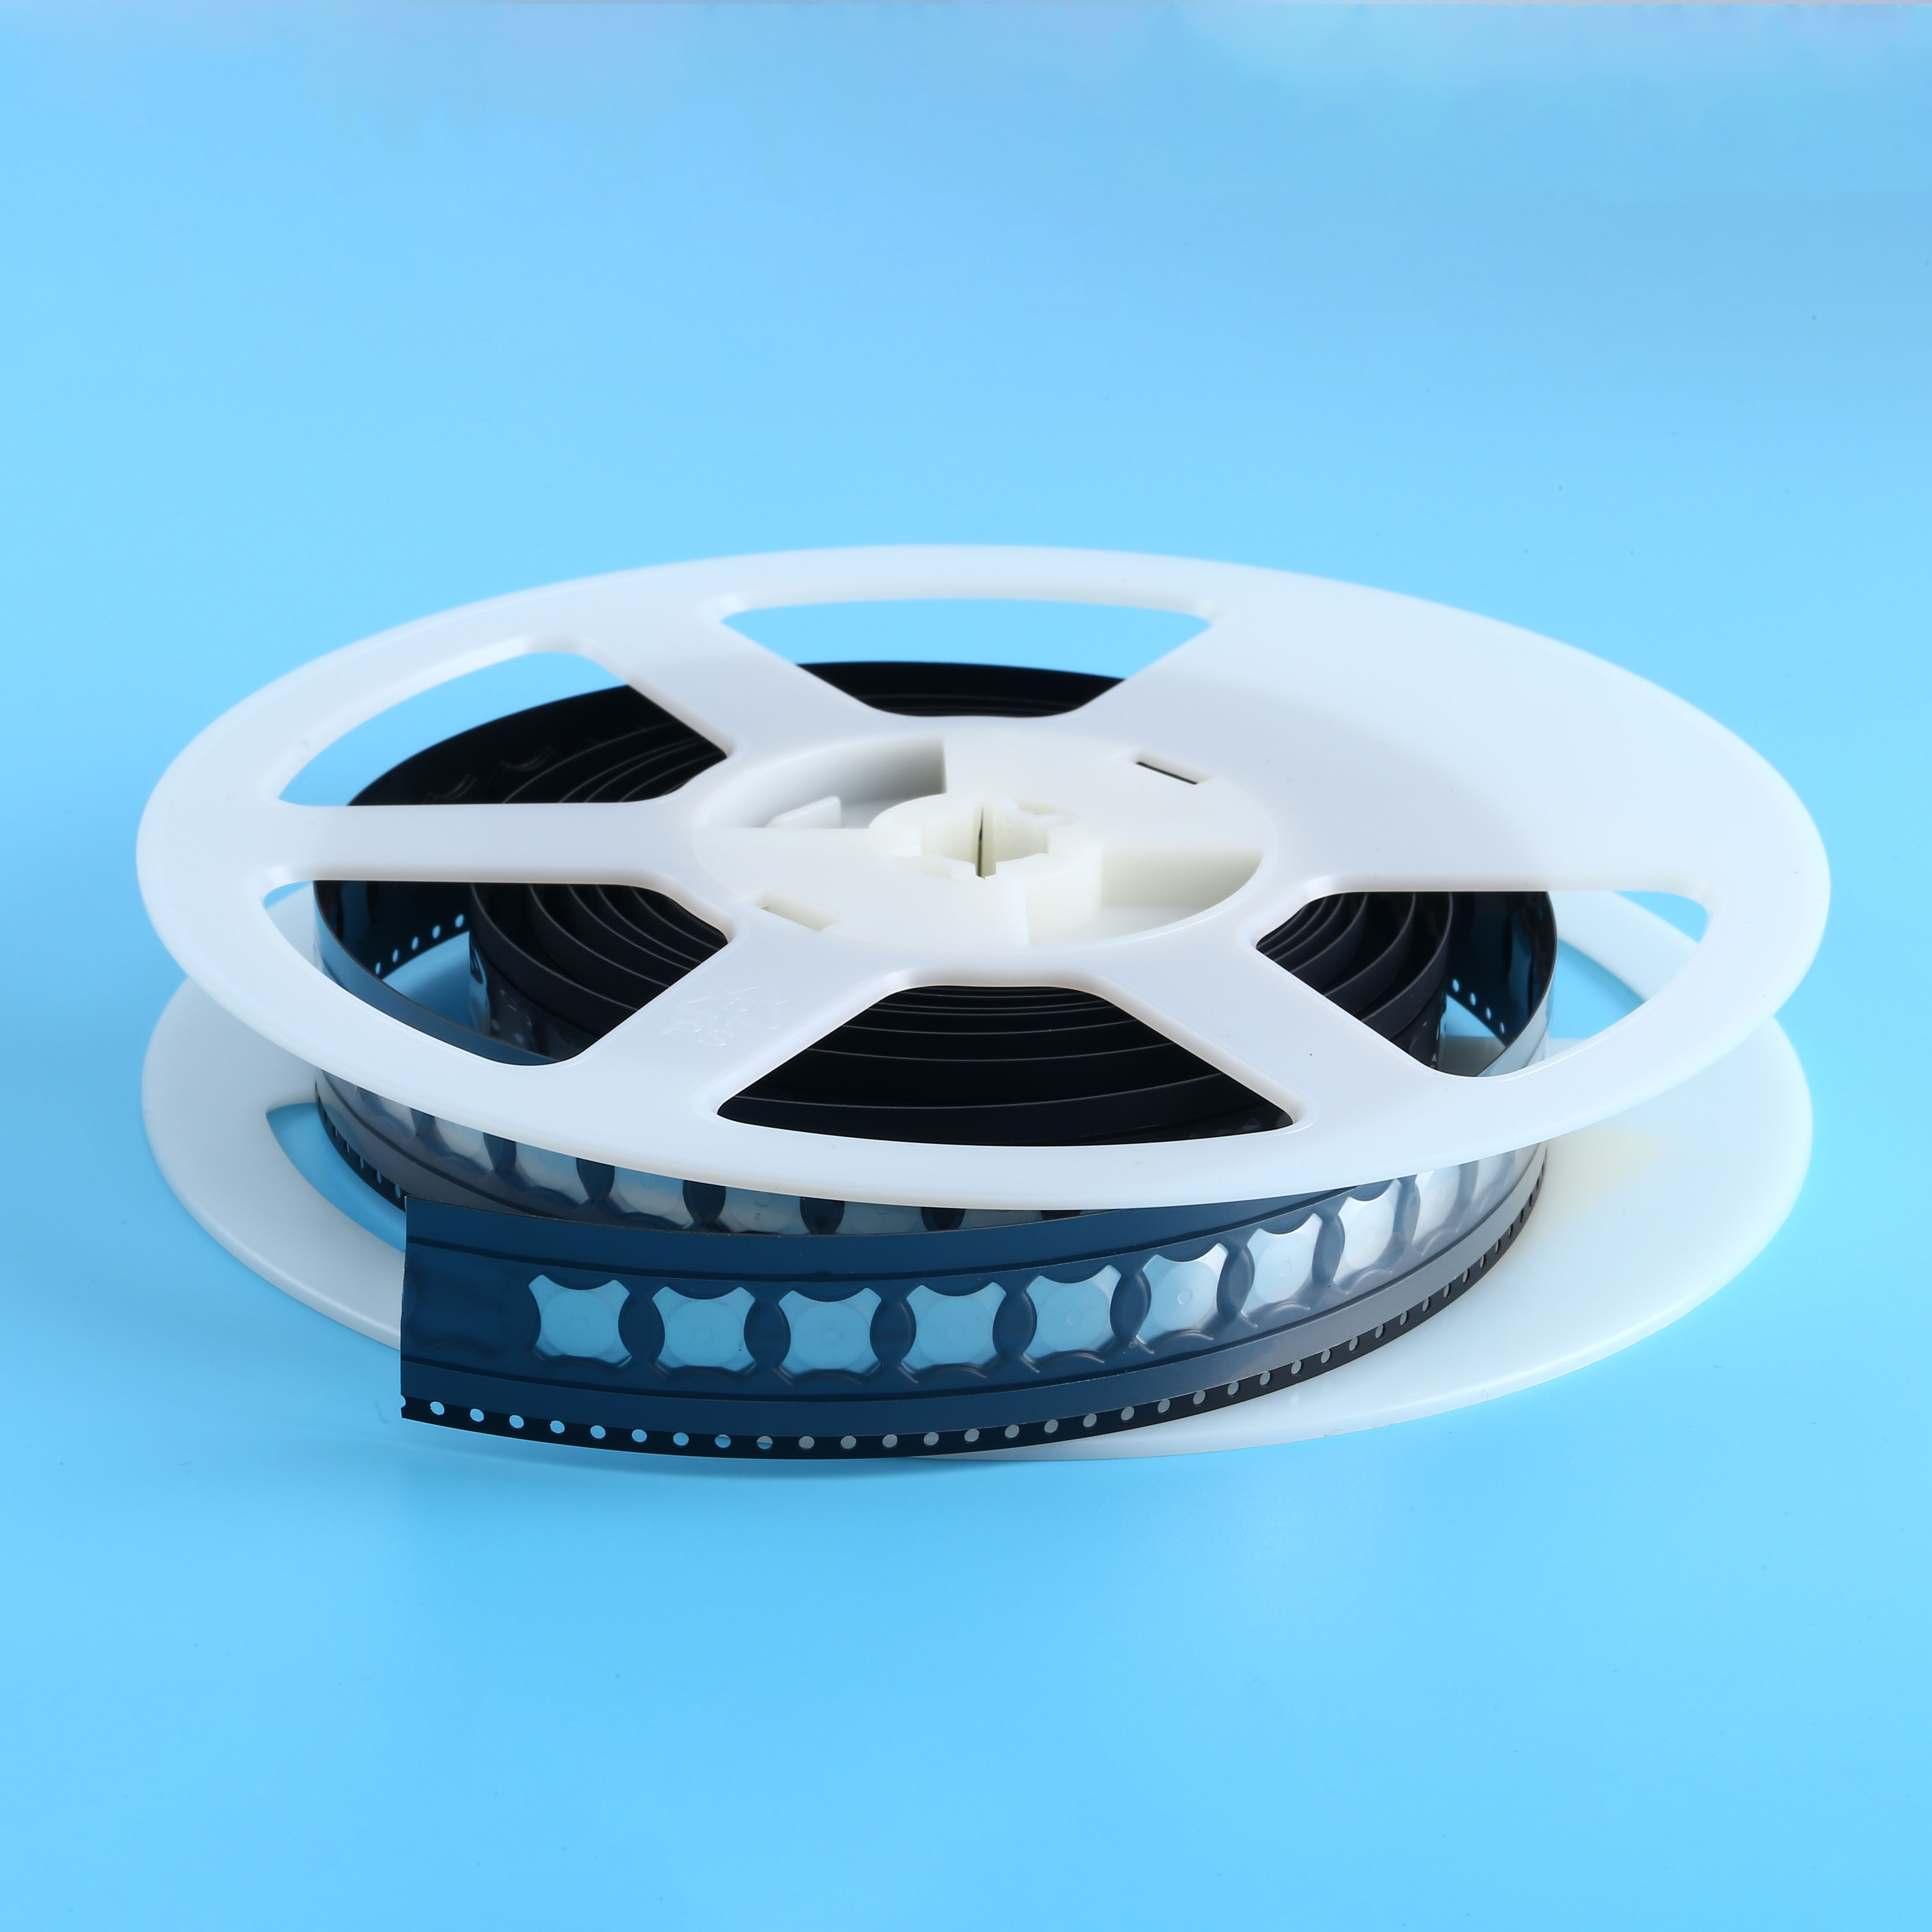
- Material: SUS301 Stainless Steel
- Contact Plating: Nickel / Selective Gold
- Air Venting: Laser-Cut Anti-Lock Channels
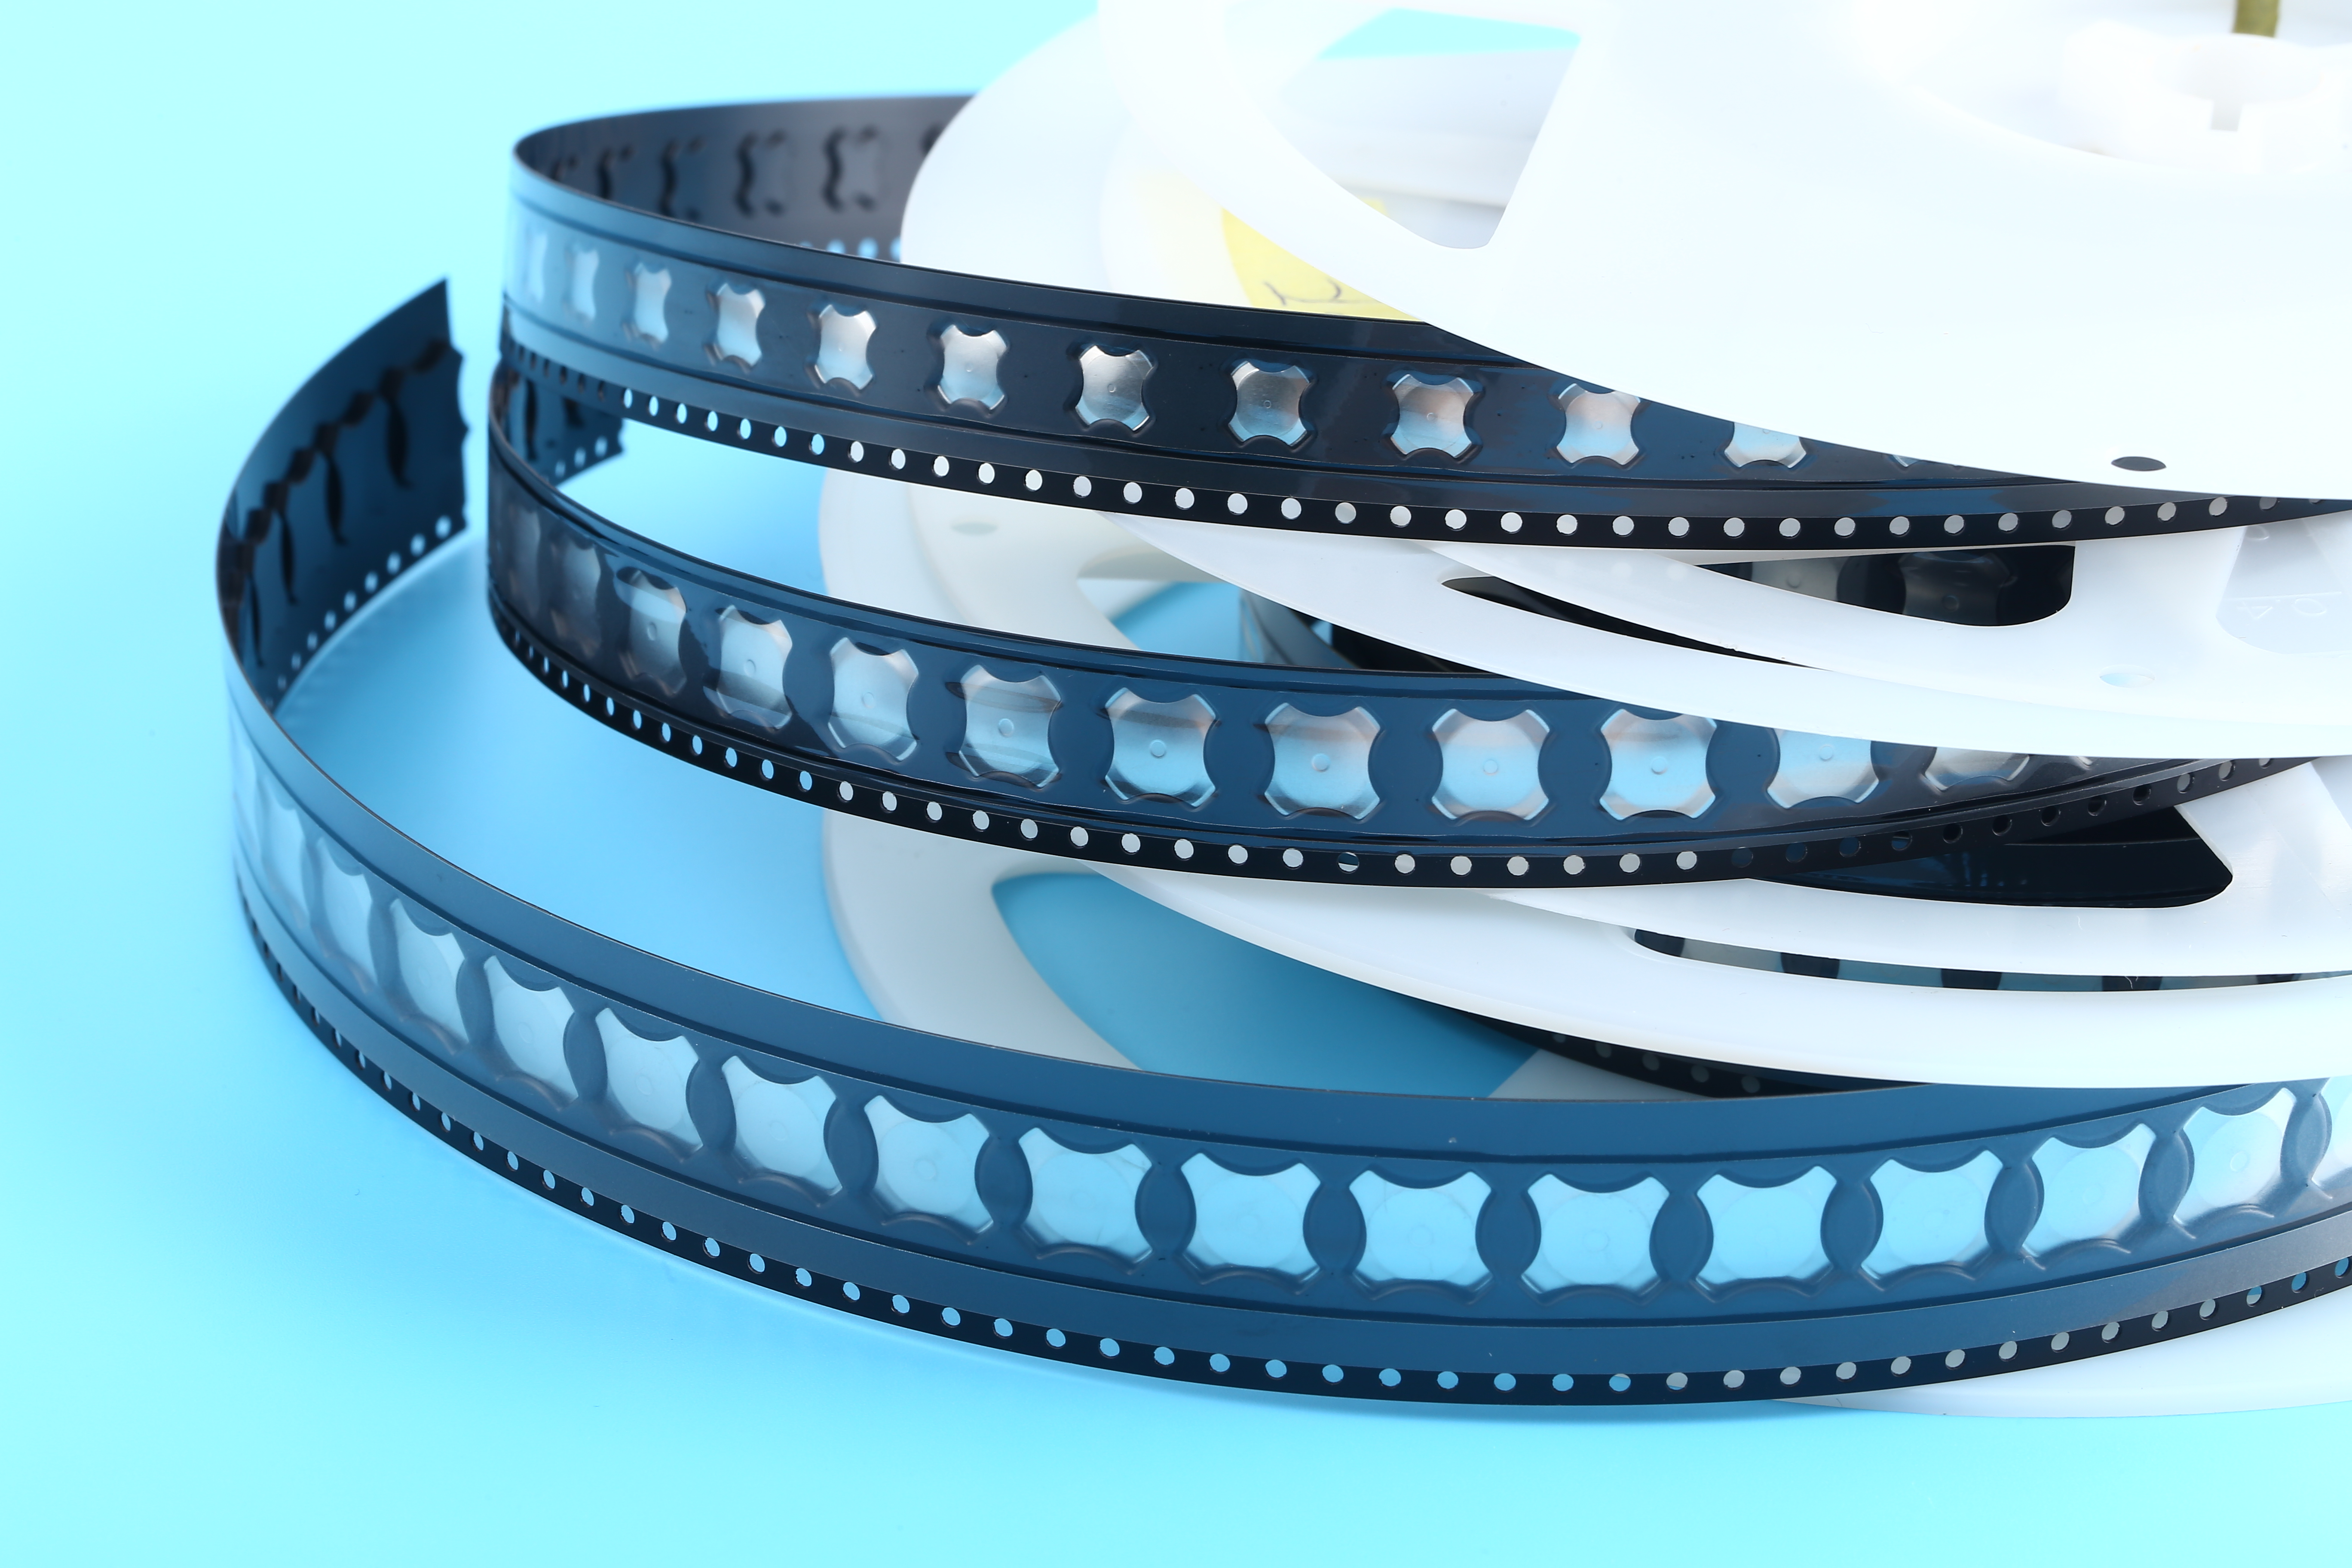
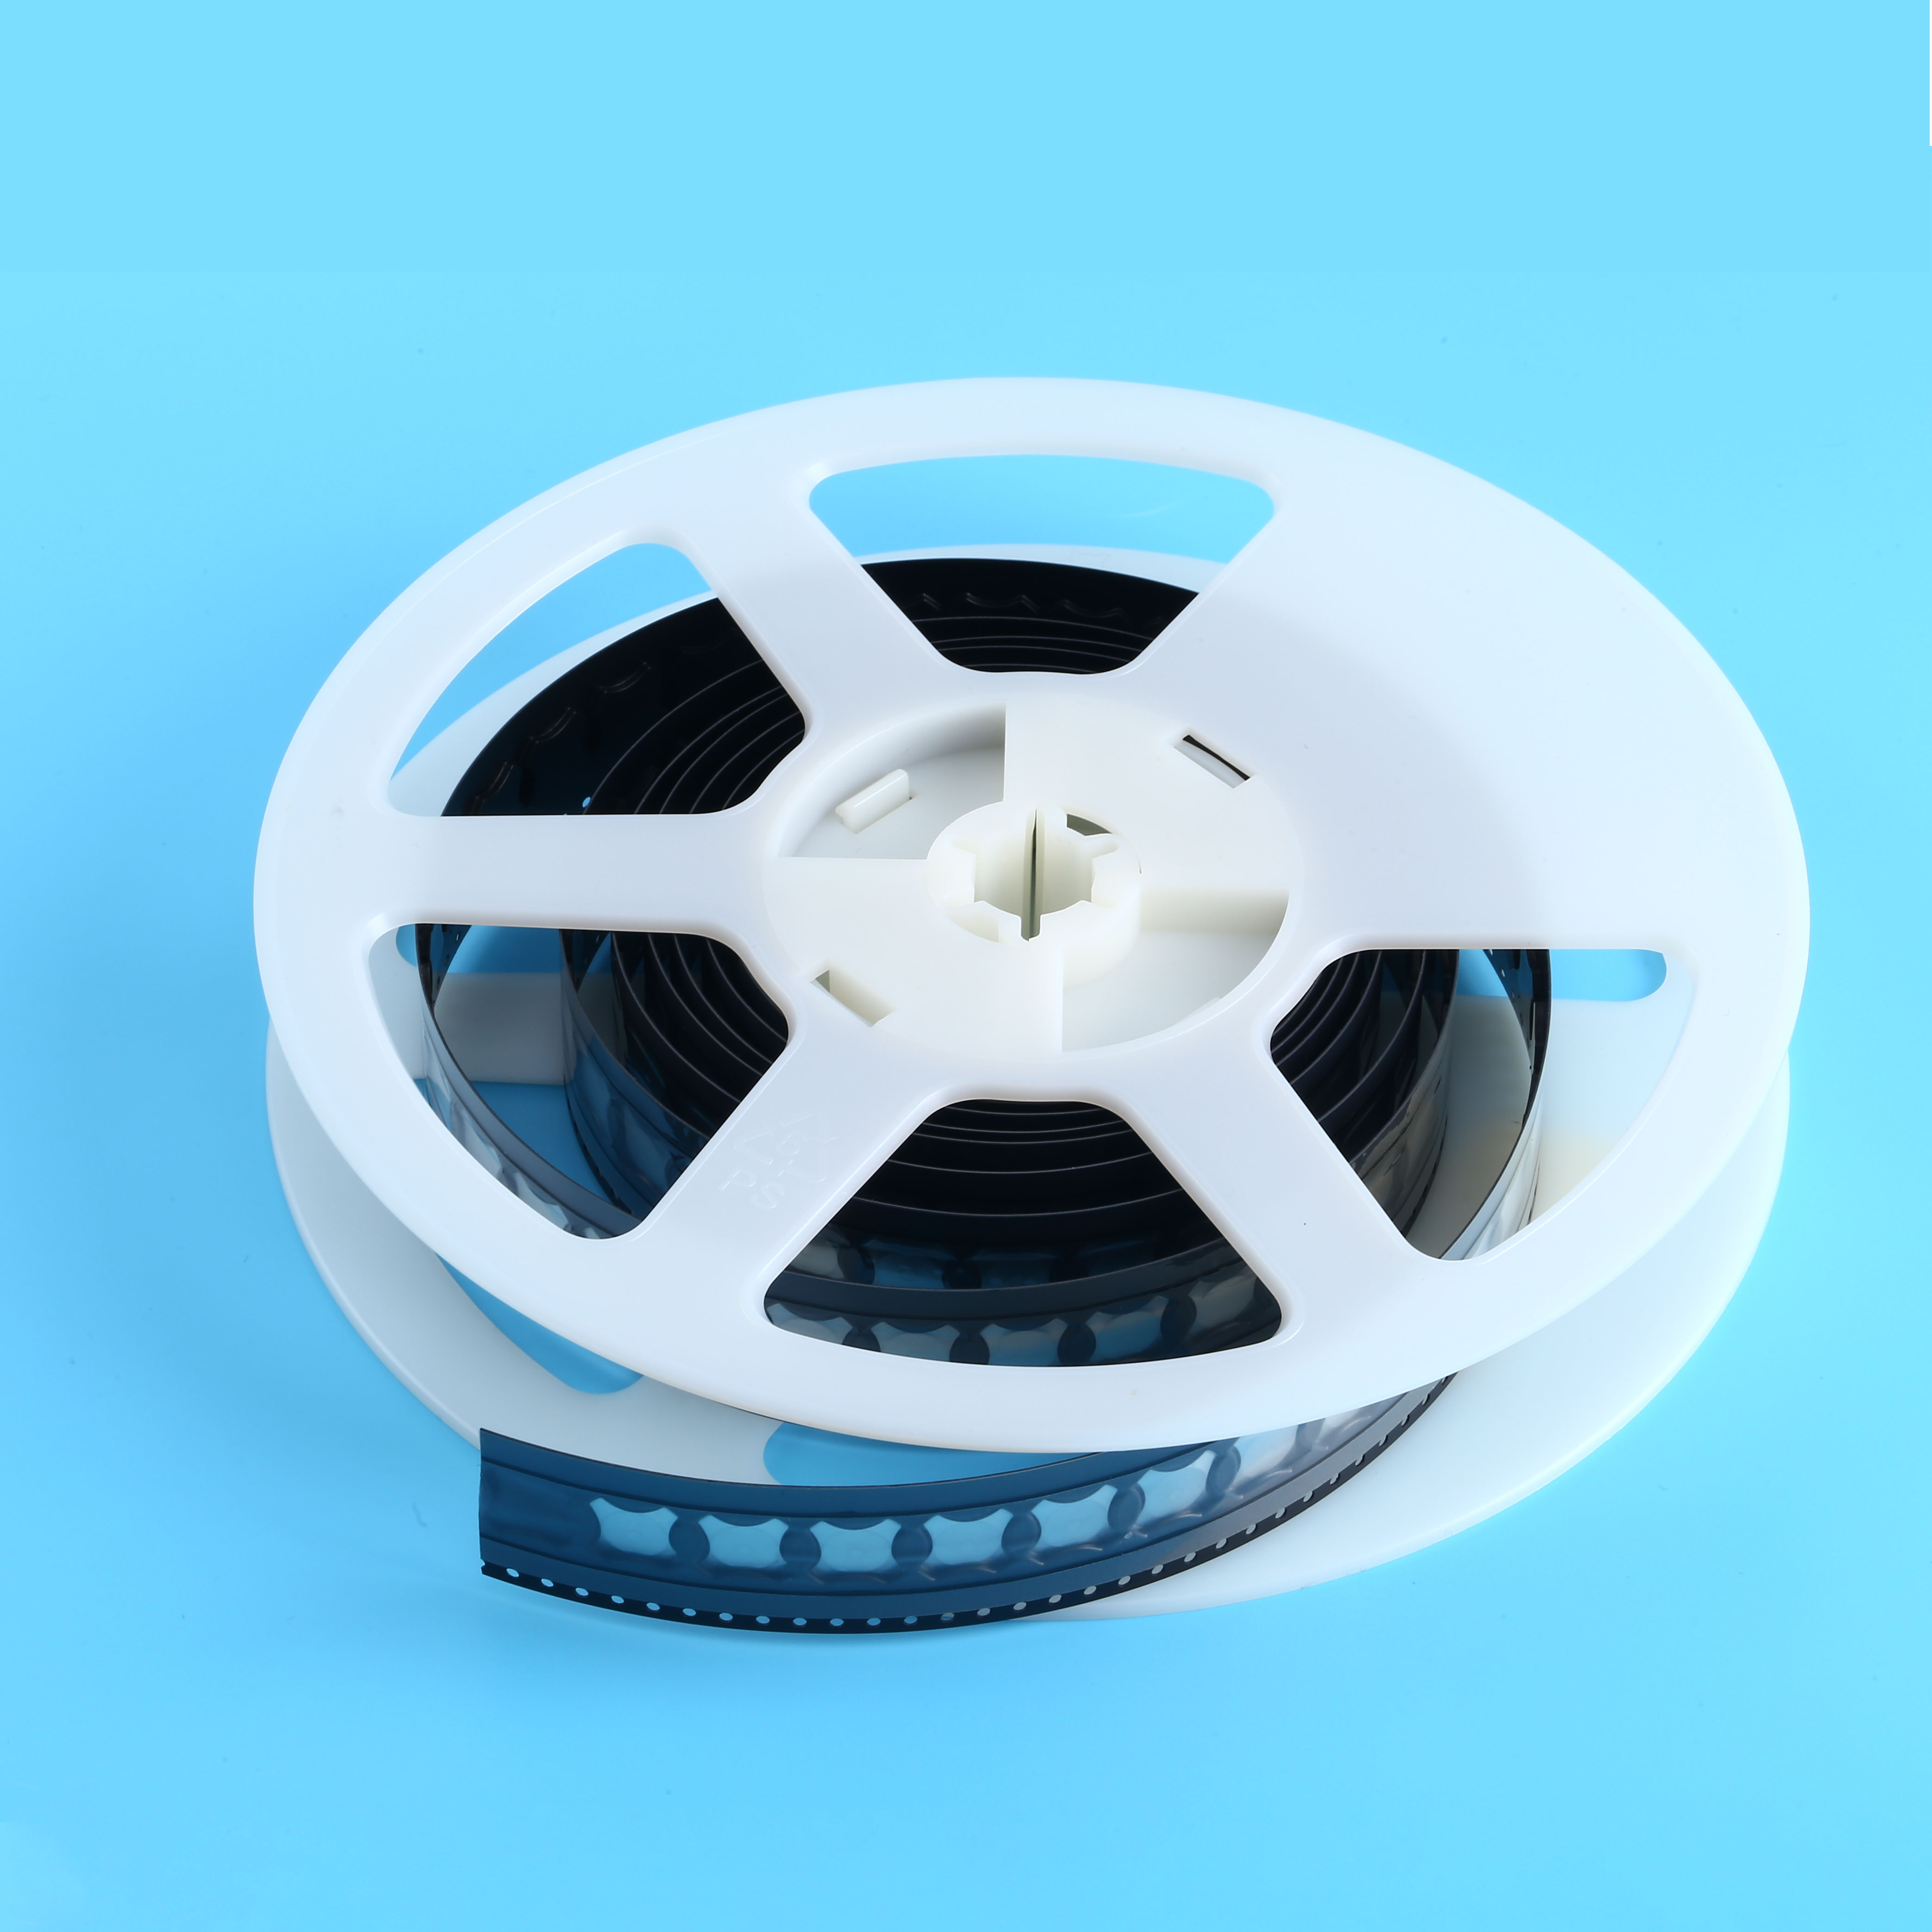
- Packaging: EIA-481 Tape & Reel
- Sizes: 6mm, 8.4mm, 10mm, 12mm
- Placement: High-Speed Pick-and-Place Compatible
- Tactile Feedback: >50% Crisp Snap Ratio
- Adhesive System: 3M 467MP / 468MP High-Bond
- Contact Resistance: < 1.0 Ohm Initial
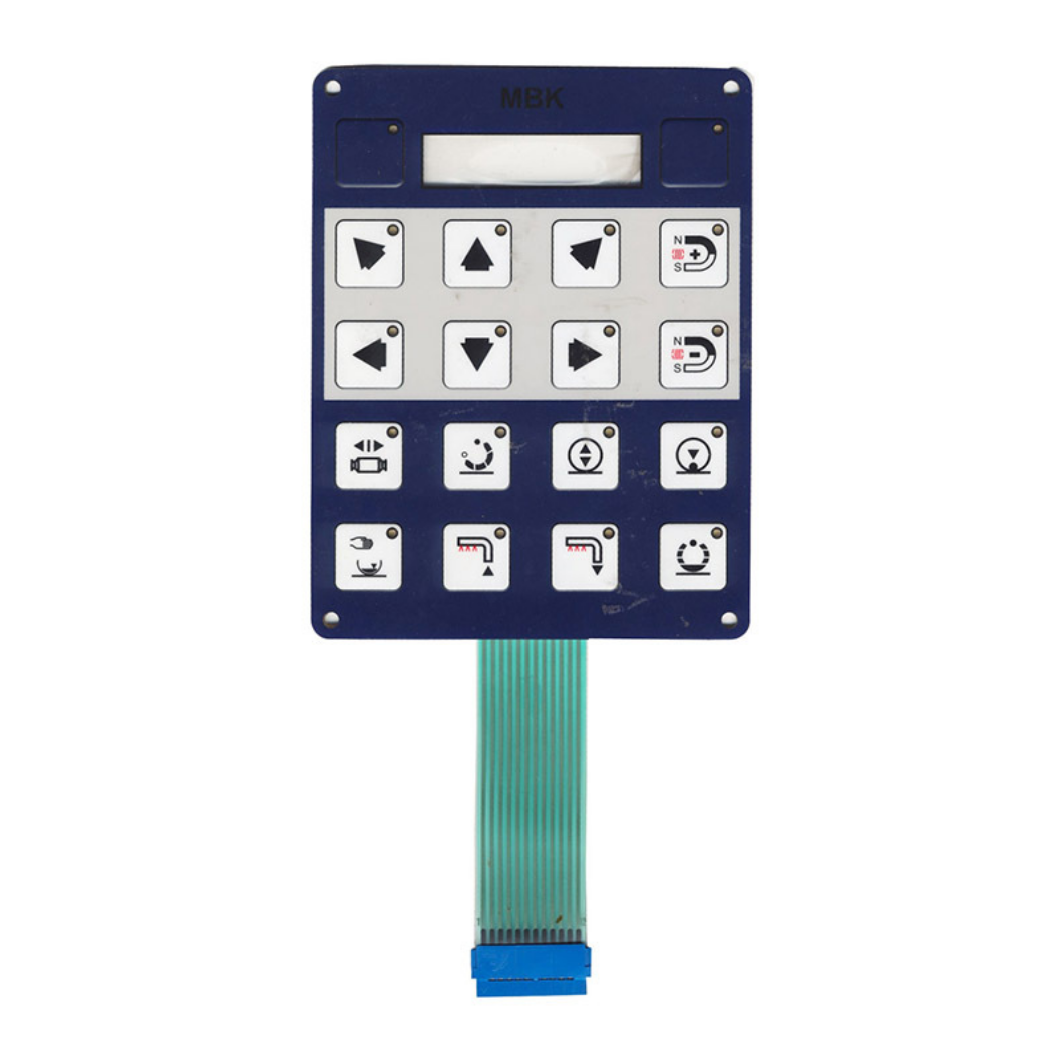
- Key Pitch: Custom Center-to-Center
- Tail Pitch: 2.54mm / 1.00mm FPC ZIF
- Embossing: Rim or Pillow Formed
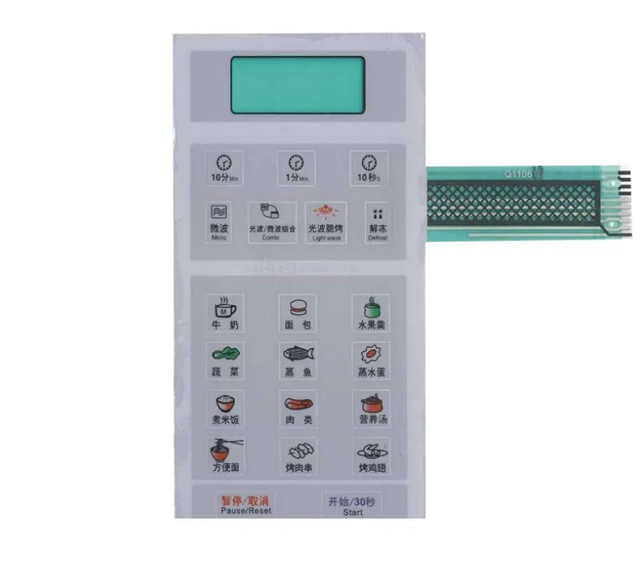
- Overlay: Autotex Hard-Coated Polyester
- ESD Shielding: Aluminum Foil / Carbon Grid
- Operating Temp: -40°C to +85°C Industrial
- Illumination: SMD Side-Emitting LEDs / LGF
- Light Uniformity: >85% Gradient Balanced
- Feedback: Audible & Crisp Tactile Click
The Limerick Market: Human-Machine Interface Requirements in Mid-West Ireland
Bridging precision manufacturing with Ireland's world-class medical technology clusters, automated manufacturing hubs, and Shannon Estuary logistics corridors.
The metropolitan region of Limerick—flanked by the vibrant industrial zones of Raheen Business Park, Castletroy, and the adjacent Shannon Free Zone—has cemented itself as one of Northern Europe’s primary advanced manufacturing centers. Historically distinguished by pioneering electronics fabrication and heavy engineering, Limerick's contemporary economic landscape is steered by high-specification Medical Devices (MedTech), pharmaceutical process monitoring, avionics maintenance, and smart agricultural machinery. For electronics procurement engineers and industrial designers operating within this market, human-machine interface (HMI) modules are not passive components; they represent the critical physical threshold between complex control circuitry and harsh operational realities.
Within this dynamic ecosystem, the transition from legacy mechanical pushbuttons or fragile exposed touchscreens to sealed metal dome membrane switches has accelerated markedly. Limerick-based design teams and contract electronics manufacturers (CEMs) face distinct environmental and regulatory requirements. Keyboards and interface panels must withstand continuous wipedowns with hospital-grade biocides (isopropyl alcohol, sodium hypochlorite, and quaternary ammonium formulations) while guaranteeing zero fluid ingress under IP65, IP67, and IP68 standards. Simultaneously, cleanroom and laboratory instruments demand an unambiguous, tactile confirmation for every operator input to eliminate erroneous data capture without requiring operators to break ocular focus from analytical displays.
MedTech & Clinical Diagnostics
Raheen and Castletroy MedTech manufacturing lines require bio-compatible, chemical-resistant PET graphic overlays with embedded antimicrobial surface coatings. The hermetically enclosed construction prevents particulate accumulation, aiding strict compliance with cleanroom protocols and ISO 13485 hygiene protocols.
- Autotex XE / MacDermid chemical-proof overlays
- Flush pillow embossing for effortless sanitization
- Zero fluid path across active switch membranes
Industrial Automation & Process SCADA
Industrial plants across the Mid-West encounter severe vibrations, electromagnetic noise from variable-frequency drives (VFDs), and extreme temperature shifts. Our switches integrate carbon/copper mesh ESD shielding (up to 15kV) to ensure uncorrupted signal integrity back to local PLCs and microcontrollers.
- ESD Shielding layer attenuation: >80dB
- 3M 468MP acrylic adhesive on powder-coated steel
- High tactile snap ratio (>50%) for gloved hands
Agri-Tech & Marine Operations
In the Golden Vale dairy processing sector and maritime tracking along the Shannon Estuary, outdoor equipment faces salt fog, prolonged UV exposure, and wide thermal cycles. UV-stabilized Polycarbonate/PET substrates resist yellowing and embrittlement over decades of continuous exposure.
- UV outdoor rating per ASTM G154 standards
- Continuous operating envelope: -40°C to +85°C
- Pressure-relief perimeter venting preserves tactility
Precision Multi-Layer Architecture of a Metal Dome Membrane Switch
Understanding the physics, mechanical actuation curves, and material selections required for zero-defect production.
A metal dome membrane switch is an intricately balanced electro-mechanical composite. Unlike elastomeric keypads or simple capacitive switches, tactile metal dome assemblies feature a crisp, non-linear tactile force-displacement curve (F-S curve). As the operator compresses the dome, force rises linearly until it reaches the critical actuation point (F1). At this point, the dome snaps instantaneously into contact with the underlying circuit pad, creating electrical continuity, while the force drops sharply to the contact force (F2). The differential between F1 and F2 defines the tactile ratio (typically tuned to 40%–65%), delivering that distinct, tactile "snap" that operators instinctively trust.
Layer 1: Graphic Overlay
Reverse screen-printed using solvent-based or UV-cured dielectric inks onto premium Autotex PET (150µm – 200µm) or Lexan Polycarbonate. Sub-surface printing guarantees keys and logos cannot be rubbed off by repeated abrasive cleaning or harsh thumb pressure.
Layer 2: Overlay Adhesive
Precision die-cut adhesive (typically 3M 467MP with 50µm film thickness or 3M 468MP with 130µm thickness) customized with laser-etched air equalization channels. These micro-vents equalize barometric shifts, preventing panel ballooning during flight or heating cycles.
Layer 3: Dome Retainer Film
An optically clear, high-tensile polyester carrier film equipped with pressure-sensitive acrylic adhesive. The retainer fixes stainless steel snap domes in precise X-Y alignment over the lower printed contact terminals, preventing lateral dome drift during continuous actuation.
Layer 4: Circuitry & Tail
Screen-printed with micro-particulate silver paste with ultra-low trace resistance (<0.05 Ω/sq), over-coated with conductive carbon to combat silver migration. Alternatively implemented on polyimide Flexible Printed Circuit (FPC) with copper-nickel-gold plating.
| Evaluation Parameter | Stainless Steel Metal Dome Switch | Non-Tactile Polydome Membrane | Capacitive Glass Touch Panel | Elastomeric Rubber Keypad |
|---|---|---|---|---|
| Tactile Feedback Feel | Crisp Audible Snap (>50% click ratio) | Muted, soft actuation (spring sensation) | Zero mechanical feedback (requires haptic motor) | Spongy, deep mechanical stroke (1.5mm - 3.0mm) |
| Glove Operation Reliability | 100% Guaranteed (Any glove material/thickness) | High reliability | Poor to Moderate (depends on glove tuning) | High reliability |
| Ingress Protection (IP Rating) | IP65, IP67, IP68 hermetically sealed | IP65, IP67 sealed | IP65 (surface only; edge seals vulnerable) | IP64 typical (requires compression bezel) |
| Actuation Lifespan | > 1,000,000 to 5,000,000 cycles | ~ 500,000 to 1,000,000 cycles | Unlimited touch cycles (fragile to impacts) | ~ 500,000 cycles |
| Tooling & NRE Startup Costs | Economical (€400 - €900 prototype tooling) | Low to Medium | High (€3,500 - €12,000 for custom molds) | Very High (€2,000 - €6,000 steel compression tooling) |
| Resistance to Hospital Cleaning Reagents | Outstanding (Impervious to bleach, IPA, iodine) | High | High (glass surface), silicone seal edges wear | Moderate (rubber tends to absorb oils/solvents) |
Key Design Trends Shaping the Limerick & European HMI Landscape
Next-generation interface innovations adopted by hardware engineering teams throughout Ireland, the UK, and continental Europe.
Integrated Light Guide Film (LGF) Backlighting
Legacy switches relied on bulky discrete LEDs or fragile electroluminescent (EL) foils with short lifespans. We now utilize micro-embossed Light Guide Films (LGF) fed by ultra-slim side-firing SMDs. This guarantees razor-sharp, non-glare symbol illumination across dark operating theaters or night-time farm cockpits with uniform lux distribution and sub-millimeter stackup.
Hybrid Capacitive + Metal Dome Switches
Limerick instrumentation designers increasingly integrate hybrid interfaces: capacitive slider or wheel sensors for variable digital parameter adjustments (e.g., fluid flow rate, oscilloscope gain), combined with physically distinct metal snap domes for mission-critical "Power", "Emergency Pause", or "Execute" functions where tactile confirmation is legally mandated.
Polyimide Flexible Circuits (FPC) with Dense Tail Routing
As medical hand-pieces and handheld field testing equipment contract in size, traditional 2.54mm pitch silver-printed polyester tails are being supplanted by polyimide FPC tails with 0.5mm and 1.0mm ZIF connector pitch. Copper-etched FPC tails allow surface-mounting of micro-controllers, thermistors, and active IC drivers directly onto the tail flex.
Why Limerick & Irish Procurement Teams Partner with Dongguan Cevra
Eliminate trading middle-men. Work directly with an audited ISO 9001:2015 precision HMI manufacturer with turnkey production under one roof.
SGS Group Onsite Verified
Our Dongguan manufacturing headquarters has undergone thorough onsite authentication by SGS Group. Production facilities, automated equipment capacity, worker counts, and enterprise authenticity are fully verified, giving Irish engineering departments total supply chain transparency.
Rapid Prototyping & DFM
Direct communication with English-speaking HMI mechanical engineers. We provide comprehensive Design for Manufacturability (DFM) reviews within 24 hours of receiving your CAD or Gerber files, providing rapid laser-cut prototypes delivered to Shannon or Dublin Airport within 5–7 working days.
Comprehensive Testing Lab
Equipped with proprietary computerized dome load testers, high/low temperature environmental stress chambers (-40°C to +120°C), adhesive peel testers, pencil hardness surface testers, and CCD automated visual alignment cameras for zero-micron trace alignment.
Flexible MOQs & Buffer Stocking
Supporting engineering projects from pilot builds (from 10 to 100 pcs) up to continuous annual runs of 500,000+ units. We offer blanket order agreements with scheduled DDP releases directly into Irish manufacturing plants, mitigating international supply line shocks.
Frequently Asked Questions by Limerick & European Purchasing Engineers
Addressing critical commercial, compliance, and engineering queries for seamless cross-border supply chain integration.
What design files and specifications are required to initiate an engineering quotation?
To provide an exact DFM analysis and production quote, please provide your mechanical drawings in DXF, DWG, PDF, or STEP format detailing outline dimensions, key cutout zones, display window locations, and tail exit coordinates. For the graphic overlay artwork, vectorized files in Adobe Illustrator (.AI), CorelDraw (.CDR), or high-res vector PDF with explicit Pantone (PMS) or RAL color codes are needed. Include functional specifications such as preferred metal dome diameter (e.g., 8.4mm, 10mm, 12mm), trip force requirement (e.g., 220g ± 30g), tail pinout matrix, operating temperature range, and connector terminal type (e.g., FCI Clincher, Amphenol Berg, or ZIF bare tail).
How do you handle shipping, customs clearance, and DDP delivery into Ireland?
We regularly ship to OEMs and electronics assemblers throughout Ireland, including Limerick, Shannon, Galway, Cork, and Dublin. We offer comprehensive DDP (Delivered Duty Paid) terms via DHL Express, FedEx, or dedicated air-cargo forwarders flying into Shannon Airport (SNN) or Dublin Airport (DUB). Under DDP, we manage export clearance, air freight, Irish customs import tariffs, VAT clearance, and inland door-to-door transit. Standard courier shipments arrive at your Limerick loading dock within 3 to 5 business days after factory dispatch.
Are Cevra products fully compliant with European Union RoHS, REACH, and CE regulations?
Yes. All raw materials deployed in our manufacturing processes—including Autotex/Lexan films, 3M pressure-sensitive adhesives, Dupont conductive silver inks, carbon resistors, and stainless steel snap domes—comply strictly with EU Directive 2011/65/EU (RoHS 2.0 / RoHS 3) and Regulation (EC) No 1907/2006 (REACH SVHC). Full material declaration certificates, safety data sheets (MSDS), and third-party laboratory test reports are provided with initial sample approvals to satisfy your internal quality and CE conformity documentation.
Which metal dome profile is best suited for gloved medical or industrial machinery operation?
For operators wearing nitrile or heavy industrial gloves, we strongly recommend our 4-legged cross snap domes (size 10mm or 12mm) with an integrated center dimple and an actuation force between 280g and 350g. Four-legged cross domes deliver a significantly higher tactile snap ratio (>50%) compared to round or oblong domes. The center dimple concentrates the downward fingertip pressure onto the primary contact point, preventing "spongy" actuation even when the operator strikes the key off-center.
Can you manufacture membrane switches with anti-microbial coatings for cleanroom diagnostics?
Yes. We frequently build overlays using specialized anti-microbial films such as Autotex AM, which features Microban® silver-ion technology integrated directly into the polyester hard-coat during film extrusion. This active biocidal protection will not wash off during cleaning cycles and permanently inhibits the growth of bacteria, mold, and mildew across 24/7 hospital, pharmaceutical, and cleanroom environments, matching the rigorous hygiene demands of Limerick’s MedTech facilities.
How does Cevra prevent silver migration and contact oxidation in high-humidity Irish climates?
Silver migration occurs when moisture and DC electrical bias cause silver ions to create conductive dendritic filaments across circuit traces, leading to premature electrical shorts. To prevent this, our production protocol specifies an over-screened protective conductive carbon layer over every critical silver circuit trace and interdigitated switch pad. Furthermore, we apply a cross-linked UV dielectric insulating mask over the entire circuit layout, excluding only the physical dome contact pads, which can also be plated in selective gold or nickel for absolute corrosion resistance.
What are your typical turnaround lead times for rapid prototypes versus mass production?
Laser-cut engineering prototype samples typically dispatch within 5 to 7 working days following digital artwork and stackup approval. For volume production orders requiring precision steel die tooling and automated lamination, standard production lead time is 12 to 16 working days. For repeat monthly call-offs, we offer consignment stock agreements or localized buffer storage schedules to enable immediate 48-hour fulfillment.
Can you laminate membrane switches onto rigid aluminum, FR4, or acrylic backer plates?
Yes, turnkey integration is a primary core capability. Rather than requiring your Limerick assembly line to manually peel and stick flexible membrane keypads onto enclosures, we supply complete turnkey front-panel assemblies. We machine aluminum, stainless steel, polycarbonate, or FR4 backer plates in-house, install PEM press-fit studs or standoffs, laminate the membrane switch with zero bubble inclusion in our cleanroom, and verify 100% electrical continuity prior to anti-static export packaging.
Ready to Engineer Your Custom Membrane Interface?
Whether you are prototyping a breakthrough medical diagnostic instrument in Raheen or upgrading rugged industrial machinery in the Shannon Estuary, our engineering team is ready to analyze your drawings, suggest optimized stack-ups, and furnish fast, competitive factory quotations.