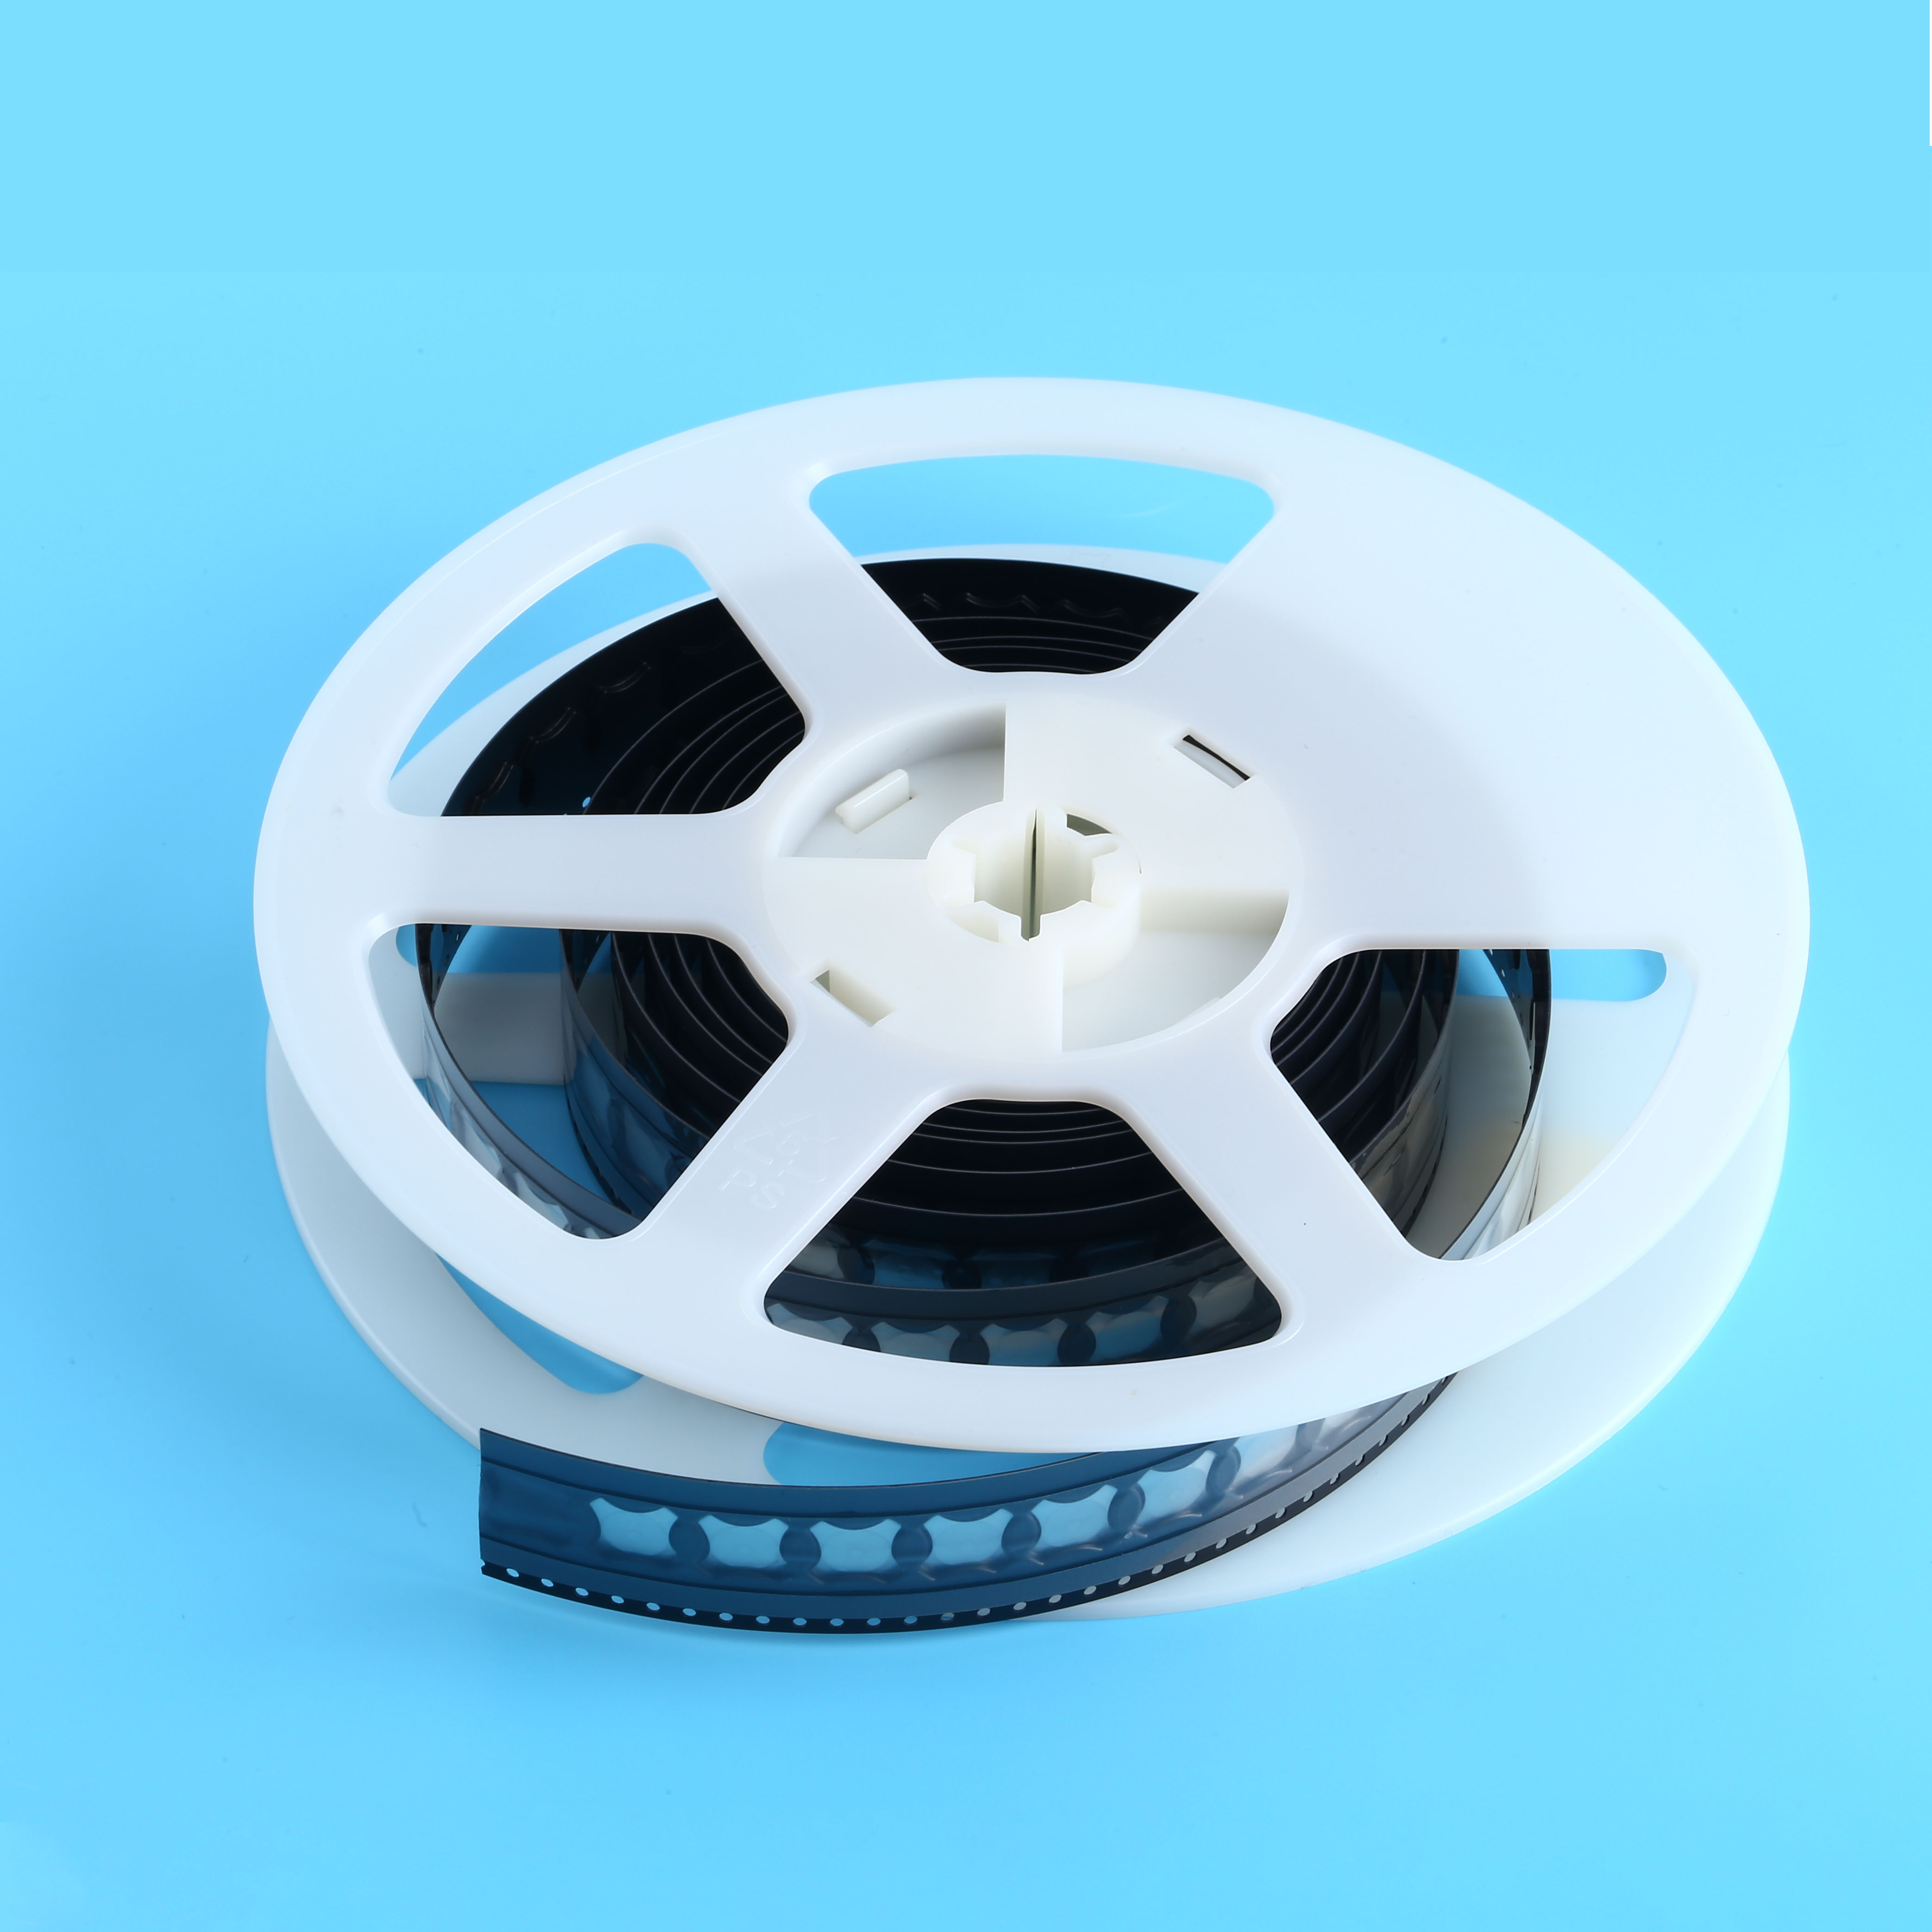
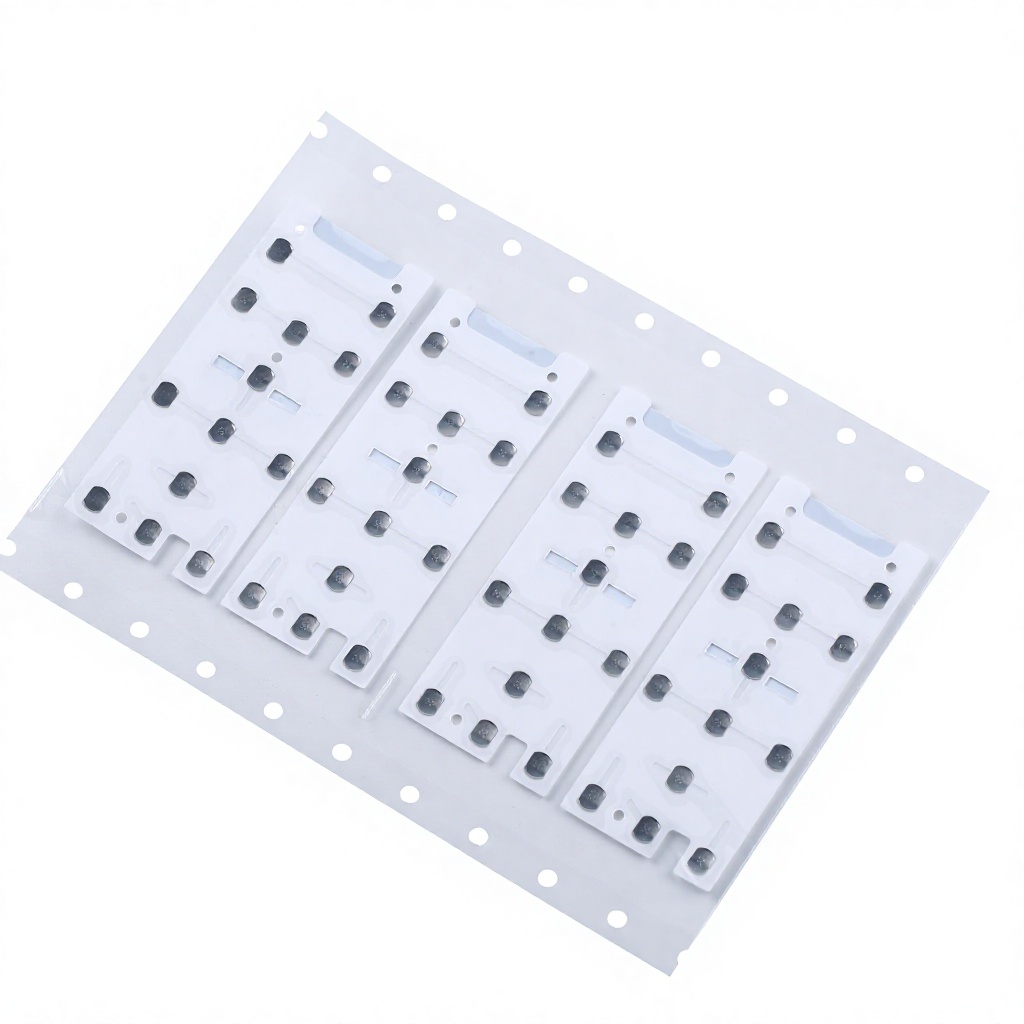
New Trend Factory Custom Cross 4-Legged Snap Dome Poly Metal Dome in Reel Packing
- Shape: 4-Legged Cross Dimple
- Packaging: Reel & Tape / Poly Array
- Material: SUS301 Stainless Steel
Explore our core product lineup: precision metal dome arrays, screen-printed graphic overlays, and sealed industrial membrane switches built to strict industrial tolerances.
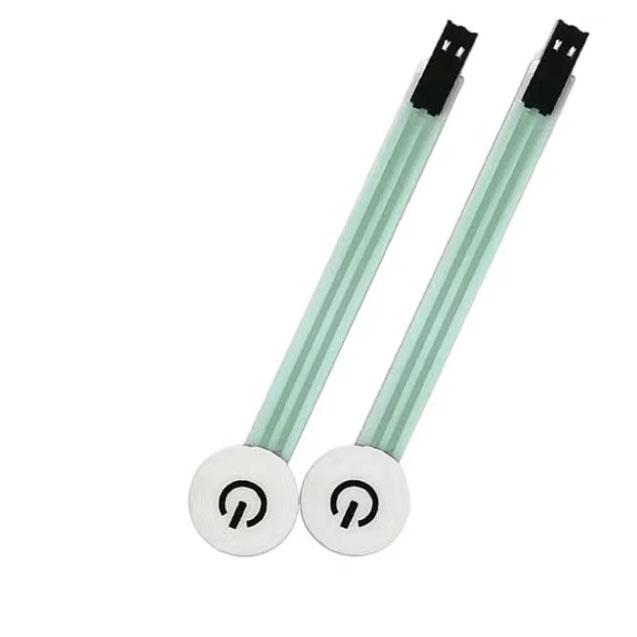
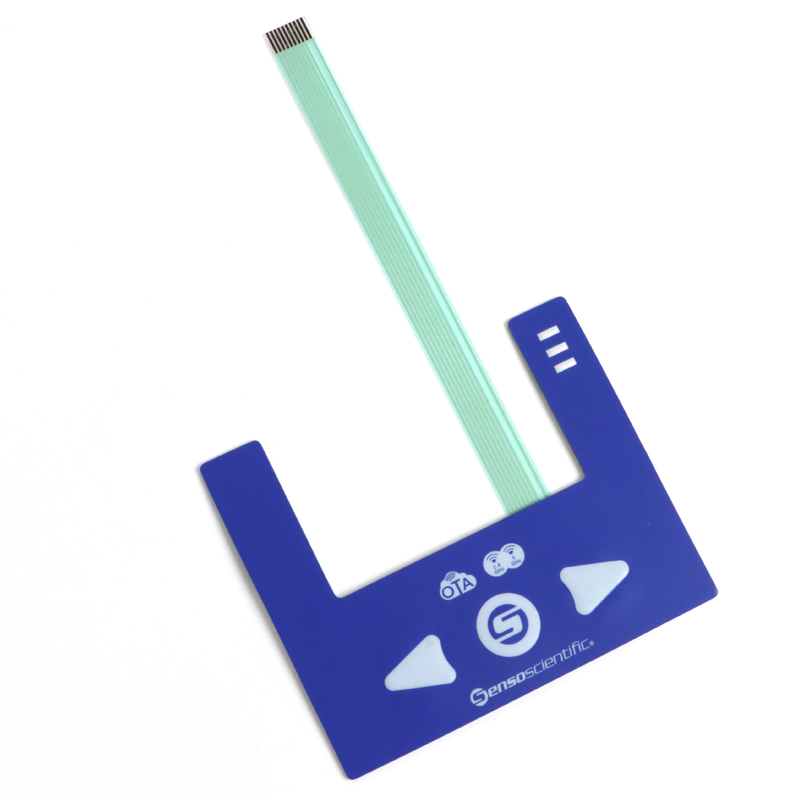
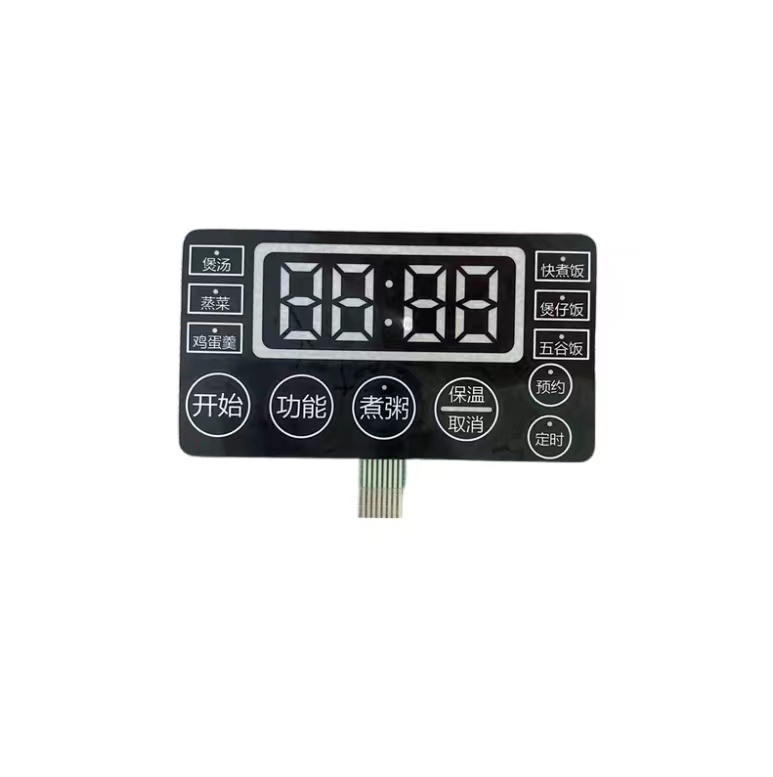
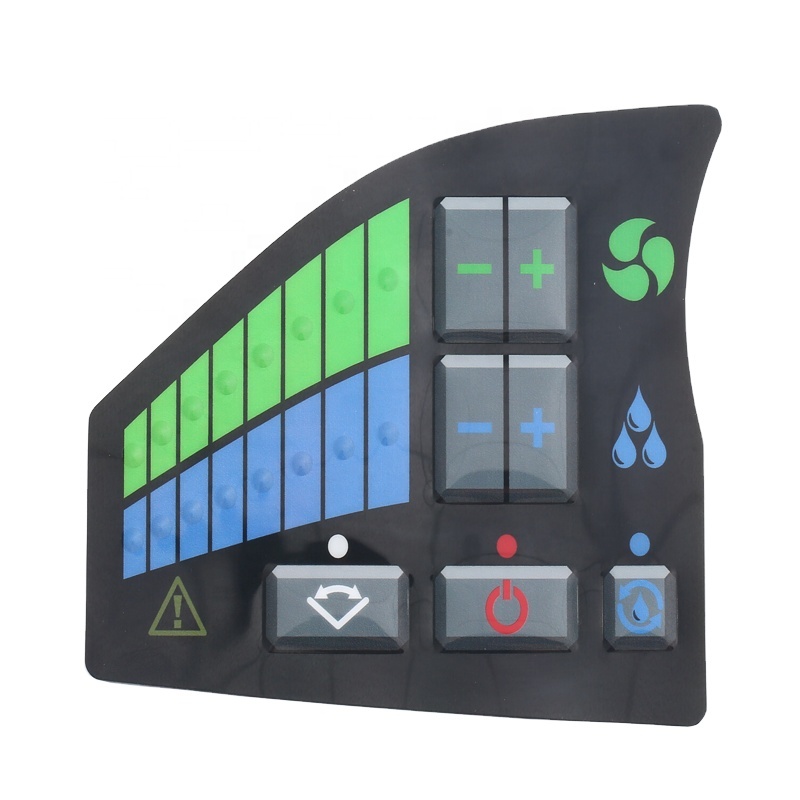
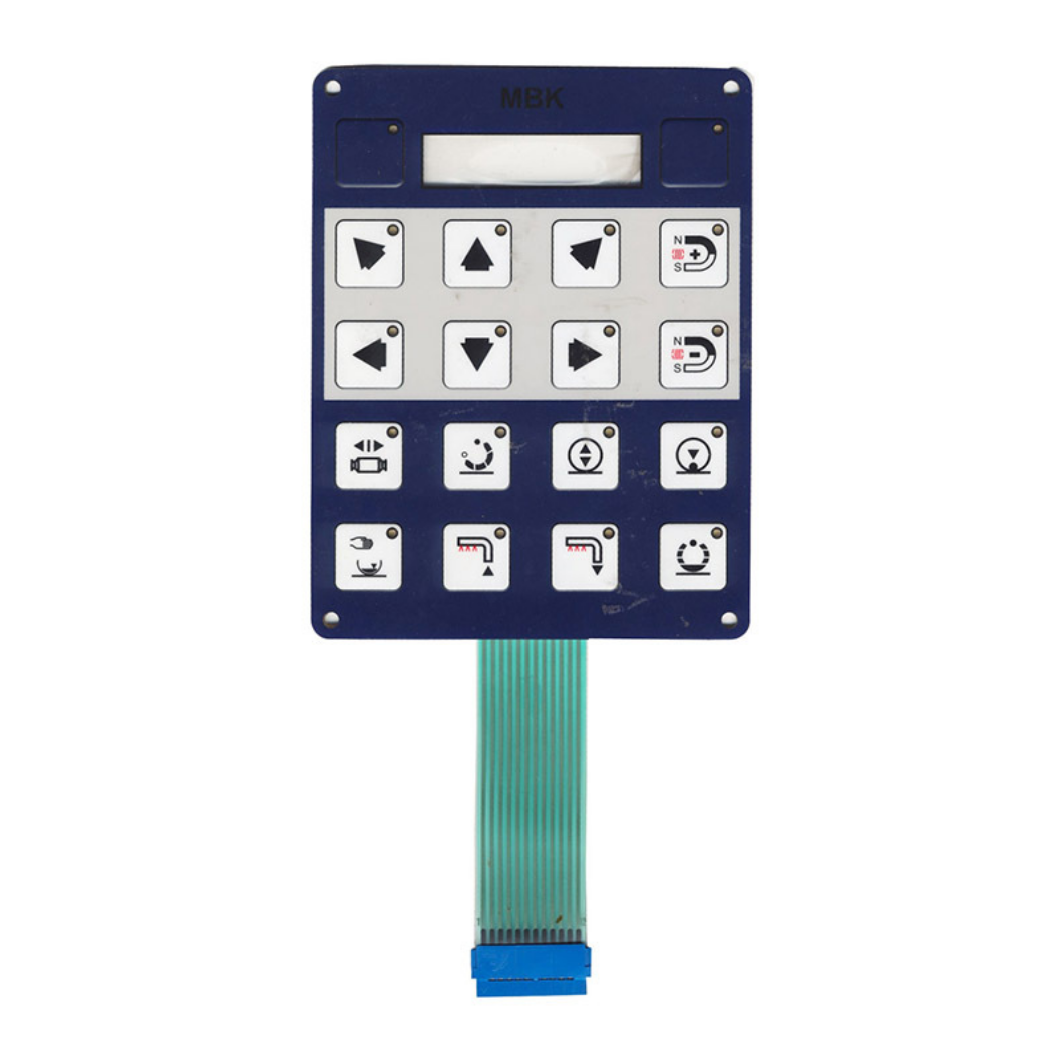
A high-performance graphic overlay serves as both the protective barrier and visual brand identity for human-machine interfaces (HMI). Cevra utilizes engineered polymer stacks designed for uncompromising durability in mission-critical applications.
Graphics, typography, and optical windows are mirrored and printed on the reverse side of transparent polymer films (PET/PC). This completely protects inks from abrasions, chemical solvents, industrial degreasers, sanitizers, and UV degradation over millions of mechanical touch interactions.
Tactile feedback and key location are enhanced via CNC-machined male-female dies. Whether perimeter rim embossing, pillow embossing, or bespoke tactile domes, our micro-forming guarantees sharp edges, uniform height (0.3mm to 0.6mm), and crack-free polymer behavior.
We apply high-performance acrylic transfer adhesives (including genuine 3M 467MP, 468MP, and 300LSE for low surface energy plastics). Adhesives are die-cut with laser precision around active keys and optical displays to prevent bubbling, light contamination, and hydraulic locking.
| Evaluation Parameter | Polyester (Autotype / Toray PET) | Polycarbonate (Lexan / Makrofol PC) | Chemically Toughened Cover Glass |
|---|---|---|---|
| Flexural Actuation Fatigue | > 5,000,000 Cycles (Zero Cracking) | ~ 100,000 Cycles (Best for non-flex areas) | N/A (Rigid substrate, zero flexural) |
| Chemical & Solvent Resistance | Superior (Resists MEK, Acetone, Bleach, Oils) | Moderate (Susceptible to aromatic hydrocarbons) | Extreme Chemical Inertness |
| Embossability & Forming | Requires thermal hydro-forming control | Exceptional cold / hot forming | Requires CNC grinding (High cost) |
| Optical Clarity & Display Windows | Good (Clear anti-glare / hard-coat options) | Outstanding Glass-Like Optical Clarity | Maximum Optical Transmission (> 92%) |
| Impact & Scratch Hardness | 3H to 4H Pencil Hardness (Hard-coated) | HB to 1H (Requires hard-coat for scratch seal) | 9H Surface Hardness (Pencil scale) |
| Cost vs Tooling Efficiency | High ROI for Medium-to-High Volume OEM | Economical for Low-to-Medium Volumes | Substantial NRE & Per-Unit Tooling |
Procurement directors and systems engineers are balancing strict budget targets against increasing field reliability requirements. Here is how forward-looking engineering teams are securing custom overlay panels for future programs.
Procurement teams are cutting bill-of-materials (BOM) complexity by sourcing integrated graphic sub-assemblies. Rather than ordering raw overlays, spacers, metal dome arrays, and PCB/FPC backings separately, buyers now specify fully validated "plug-and-play" turnkey panels directly from Cevra.
To guard against global supply bottlenecks, tier-one manufacturers partner directly with ISO-certified factory floors in Dongguan that maintain end-to-end tooling, CCD screen printing, and die-cutting in-house, bypassing costly trading intermediaries and cut lead times by 40%.
Global regulatory pressure mandates full RoHS 3.0, REACH, and Halogen-Free certifications across all materials—from sub-surface pigments and silver conductive traces to acrylic adhesive liners. Factory audits by SGS provide direct compliance evidence for enterprise supply chains.
High-mix, low-to-medium volume (HMLV) programs demand low initial commitments. Cevra bridges the gap with digital UV flatbed proofing and laser prototyping from as low as 10 pieces, moving directly into high-precision hard-tooled mass production without friction.
The standard graphic overlay is evolving from a passive aesthetic faceplate into an active, intelligent electro-mechanical component. Stay ahead of interface design with these critical technological shifts.
Combining traditional sub-surface graphic overlays with printed capacitive sensor matrices allows completely sealed, zero-gap flat front panels. These interfaces eliminate mechanical wear points, achieve true IP68 liquid ingress ratings, and support multi-touch and gesture control through thick plastic enclosures.
Bulky EL lamps and high-profile LEDs are being replaced by micro-etched Light Guide Films (LGF) as thin as 0.125mm. Powered by edge-mounted surface-mount (SMT) side-firing LEDs, LGF delivers exceptionally uniform backlighting across keys and legends with ultra-low power consumption and zero thermal buildup.
Medical ventilators, food processing lines, and outdoor industrial monitors require active surface protection. Cevra applies specialized textured hard-coats with embedded silver-ion antimicrobial agents (inhibiting 99.9% of bacterial growth per ISO 22196) and non-yellowing fluoropolymer films resistant to continuous outdoor UV exposure.
Established in March 2009 in Dongguan, China, Cevra is an authentic ISO 9001:2015 certified manufacturer with 2,600㎡ of self-operated clean workshops, fully automated printing, laminating, and 100% QA inspection.
Our workshop, production capacities, skilled labor force, and QA procedures are independently audited and verified on-site by SGS Group. Buyers enjoy complete provenance and zero trading risk.
We do not outsource critical operations. From automatic screen printing, CCD alignment punching, precision laser die-cutting, to automatic lamination and dome positioning, every stage is fully controlled in-house.
Every production batch is validated against metal dome load force testers, high/low temperature humidity chambers (-40°C to +105°C), tension/peel adhesive testers, holding tack fixtures, and pencil surface hardness testers.
Direct communication with experienced DFM (Design for Manufacturability) engineers fluent in English. We review your CAD, DXF, or AI files, verify layer clearances, and propose stack-ups that optimize cost and reliability.
Essential answers regarding material selections, manufacturing limits, minimum orders, and reliability testing for custom graphic overlay and membrane panel sourcing.
To deliver an accurate quotation and DFM analysis, we accept vector artwork in Adobe Illustrator (.AI, .EPS), AutoCAD (.DXF, .DWG), or vector PDF format. Your files should separate graphic artwork layers, die-cut vector cut-lines, embossing locations, display window positions, and selective adhesive coverage. Additionally, please provide your target Pantone (PMS) or RAL color codes, operating environment parameters, and required tactile feedback type (e.g., flat, metal dome, or poly-dome).
The choice between PET and PC depends entirely on the mechanical, chemical, and operational demands of your end application:
Choose Polyester (PET) if the overlay incorporates actuated keys with metal domes or embossed keys subject to repetitive mechanical flexure. High-grade PET (such as MacDermid Autotype) withstands over 5,000,000 actuations without flexing fatigue, white-line crazing, or cracking. It also provides outstanding chemical resistance against aggressive solvents, bleach, and industrial oils, making it the industry standard for medical devices and industrial machinery.
Choose Polycarbonate (PC) if the application requires deep thermal hydro-forming, 3D contour shapes, or optical display clarity with zero haze. PC offers excellent flammability ratings (UL94 V-0 or V-2 options) and is economical for flat or non-flex panels. However, standard PC is more vulnerable to solvent attack and flexural fatigue over long operational lifespans unless treated with specialized hard-coats.
We manufacture 4-legged cross domes, round snap domes, and triangular metal domes in stainless steel (SUS301) with contact finishes in bare stainless, nickel, or selective gold plating. Standard diameters range from 4mm up to 20mm, with actuation trip forces precision-calibrated between 160g and 500g. Every production run is audited on automated metal dome load-force deflection testers to ensure trip force, switch travel, and snap-ratio remain tightly within ±15g of engineering specifications.
Achieving reliable ingress protection requires engineering a continuous perimeter adhesive ring surrounding all internal circuits, domes, and optical cutouts. We utilize closed-cell acrylic foams and high-cohesion transfer tapes (such as genuine 3M 467MP, 468MP, or 3M 300LSE for powder-coated or LSE plastic housings). We also design air-relief channels (vent paths) running directly between tactile key pockets, venting internal pressure differentials back into the enclosure housing without exposing the perimeter to environmental ingress.
Because we operate flexible in-house manufacturing, our prototype minimum order quantities for custom graphic overlay keypads begin at just 10 pieces for design verification runs. Standard custom production batches generally begin at 100 pieces for membrane switches, and 1,000 pieces for loose or reel-packaged metal domes. Prototype lead times typically run 5 to 7 business days following artwork and stack-up sign-off; volume mass production runs ship within 10 to 18 business days.
Yes. We integrate ultra-thin surface-mount (SMT) chip LEDs (0603 or 0805 packages) directly onto flexible conductive layers using conductive silver epoxy and UV encapsulation. For optical display windows, we produce crystal-clear windows, anti-glare matte windows, color-tinted filter windows (e.g., green, red, smoke), and "dead-front" effects. In dead-front designs, graphics or indicator symbols remain completely black and invisible until illuminated by the underlying LED backlight.
Every batch of graphic overlays and membrane switch assemblies undergoes rigorous protocol testing in our in-house QC laboratory:
1. 100% Automated Electrical Check: Automated testers verify loop circuit resistance, insulation resistance (> 100MΩ at 100V DC), and contact bounce (< 5ms).
2. Optical & Dimensional CCD Inspection: Automated optical inspection measures printing registration, key pitch, and perimeter die-cut tolerances (±0.05mm).
3. Adhesion & Tensile Testing: ASTM D3359 cross-hatch ink adhesion checks, along with 180° peel adhesion testers for 3M adhesive strength.
4. Environmental Stress Testing: High/low temperature storage (-40°C to +85°C) and constant humidity (95% RH at 40°C) thermal cyclic evaluation.
Industrial interface overlays and dome arrays are sensitive to mechanical creasing and static accumulation. All products are vacuum-sealed in anti-static ESD bags with silica desiccant pouches. They are packed flat between rigid corrugated stabilizer boards with protective non-abrasive interleaving films between every layer. Outer master cartons are reinforced with edge protectors and wrapped in moisture-resistant stretch film to guarantee perfect arrival via air express (DHL/FedEx) or ocean freight.
Connect with our technical design team in Dongguan. Send your engineering drawings or specification sheets for an immediate DFM manufacturability review, material recommendations, and a rapid quotation.